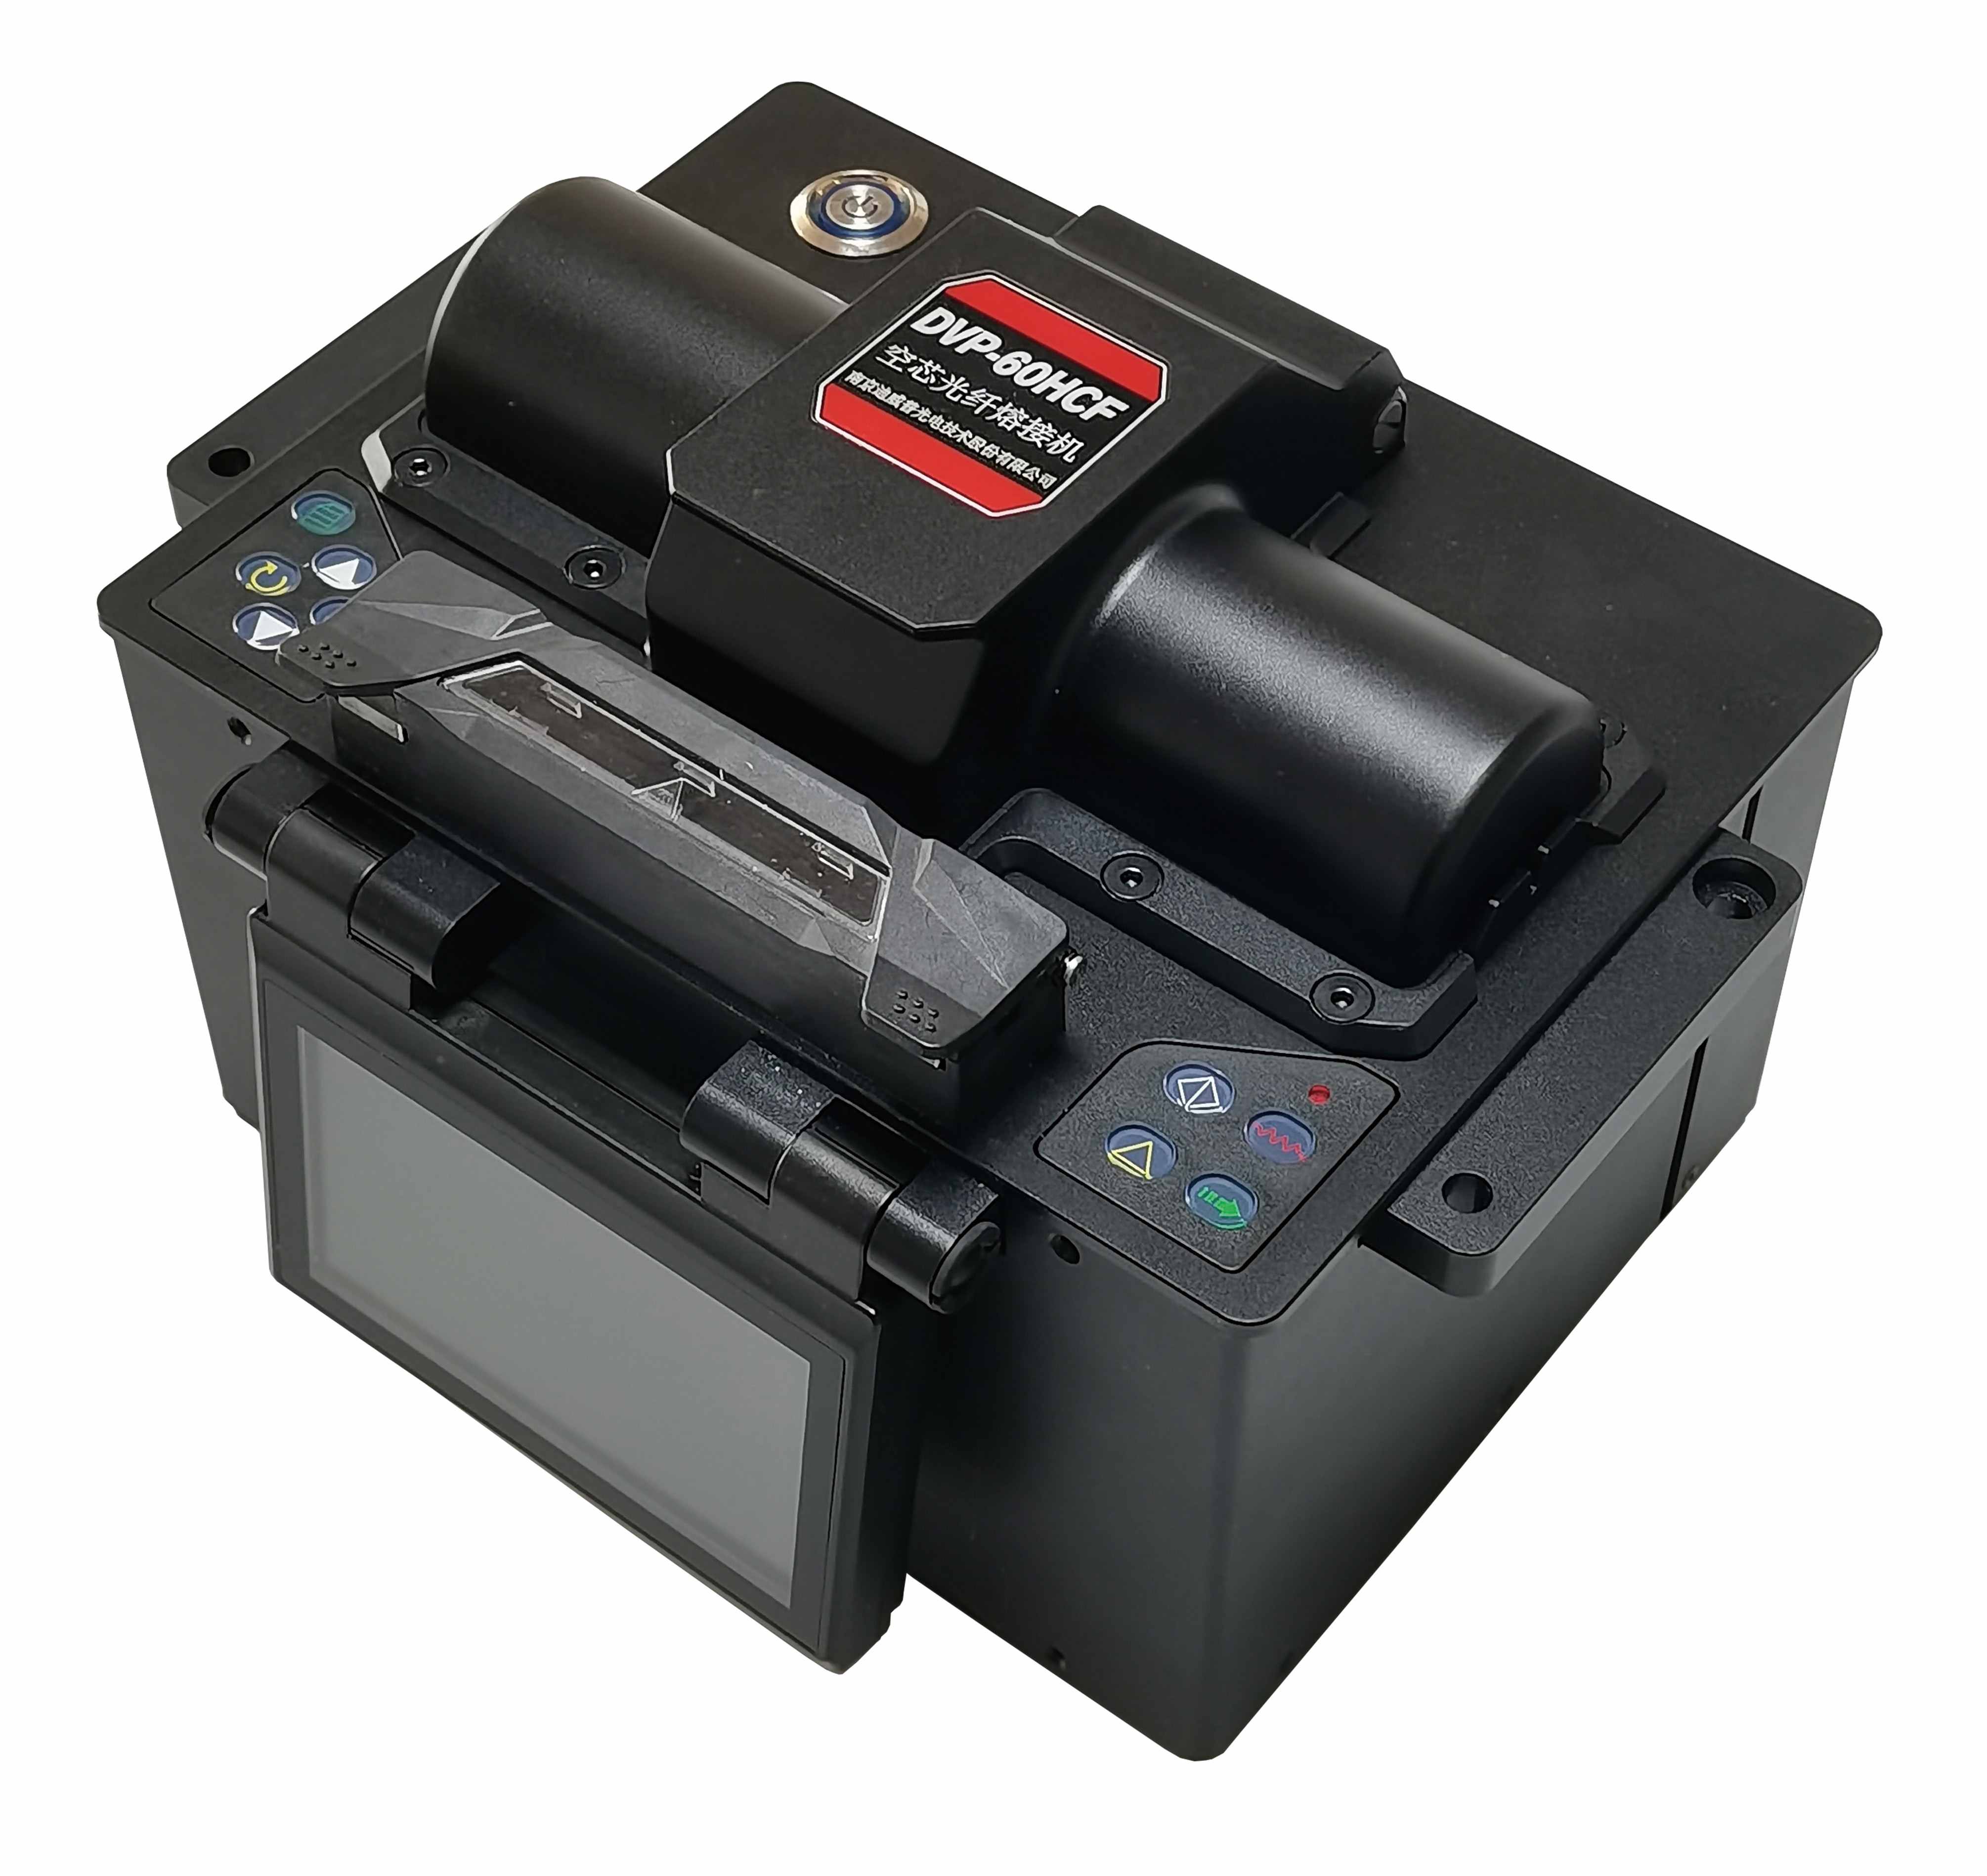
Hollow Core Fiber Fusion Splicer Factory Manufacturing Excellence
2026-08-14
As optical networks push toward lower latency and higher power thresholds, hollow-core fibers have moved from lab curiosity to commercial necessity—yet splicing them remains a bottleneck few manufacturers dare to tackle. At DVP's dedicated fusion splicer factory, that challenge is met with obsessive alignment algorithms, sub-micron electrode control, and a production line built around zero-defect tolerance. This post takes you inside the manufacturing floor where every splice loss, every arc calibration, and every thermal stress test is engineered to turn fragile air-core geometry into field-ready reliability. Curious what separates a prototype splicer from a factory-hardened workhorse? Keep reading.
Where Light Gets a Clear Path
There is a particular kind of stillness that comes when light is allowed to move without interference. Not the harsh beam of a spotlight, nor the washed-out glow of an over-lit ceiling. It's the kind of light that finds its own way around a room, tracing the edges of a table, slipping between chair legs, pooling softly on a wooden floor. This is light with a clear path—unhurried, deliberate, and surprisingly intimate.
Creating that path often means subtraction rather than addition. Removing heavy lampshades that trap brightness, repositioning a fixture so it doesn't bounce off a mirror the wrong way, or simply leaving a window uncovered during the hours when the sun sits low. The result is a quality of illumination that feels less like an effect and more like a natural condition of the space. You stop noticing the light source and start noticing what it reveals: the grain of a shelf, the texture of a woven throw, the quiet color of a painted wall.
At the end of the day, a clear path for light changes the way a room breathes. It softens hard edges, deepens shadows just enough to give shape, and keeps the air from feeling flat or sterile. The space doesn't ask for attention; it simply feels right. And that, more than any technical measurement, is what makes the light worth paying attention to.
Precision That Begins Below the Micron
Below one micron, the usual safety margins disappear. A spindle that runs warm by a few degrees can expand steel enough to erase a 0.5 µm clearance, while a floor vibration from a passing cart shows up as a jagged line on the surface profile. So the real work happens in the choices that never appear on a drawing: granite bases with tuned damping, temperature-compensated scales, and toolpaths that account for the machine's own elastic deflection mid-cut.
Inspection at this scale also changes meaning. A single average roughness number can hide a 200 nm burr folded into an edge, or a periodic waviness that only appears under a narrow band of light. The practical approach is to look at the surface the way it will be used—contact stress, sealing, optical reflection—and map the microgeometry accordingly. That is the difference between a part which measures in spec and one that actually works when it matters.
The Quiet Craft Behind Every Splice
A splice rarely announces itself. It sits under paint, inside a cable, or between frames, and its only job is to hold when everything else moves. The hands learn what the eyes cannot: a thread's willingness to bend, a wire's memory of tension, the exact point where two edges stop fighting and start agreeing. The room stays almost silent, except for the small click of material finding its place.
Every join has its own temperament. One length of rope might accept a twist on the first try; another needs to be coaxed, loosened, then drawn tight again. There is no universal method, only a kind of dialogue that develops over years. Mistakes are not failures—they are the material telling you where its limits are. That feedback loop is what turns a mechanical task into a craft.
The quiet craft behind every splice doesn't ask for recognition. It thrives in the moments between idea and result, where patience substitutes for spectacle. A well-made splice is easy to overlook because it makes the finished object seem inevitable. But the maker knows better: that small, deliberate act is what keeps the big, visible parts from coming apart.
Building the Core, One Layer at a Time
Most people try to build strength by piling on everything at once, but a real core grows the way sediment turns to stone—one deliberate layer at a time. The first layer is always the least glamorous: a stable foundation of basic control and honest assessment of where you actually are, not where you want to be. Without that, every future layer rests on sand.
Each new layer then has to bond with the one below it before you even think about adding more. That means repeating simple movements until they feel boring, then adding a slight variation—a few extra seconds, a narrower stance, a slower tempo. The goal isn't to stack as many layers as possible in a week; it's to make each layer so inseparable from the last that the whole core starts to behave like a single, unified piece.
What surprises people is how quickly a patient, layered approach catches up to—and then surpasses—a frantic one. By the time you're ten or twelve layers deep, the core isn't just strong; it's adaptable, because it was built with thousands of tiny corrections along the way. You stop thinking about layers altogether and simply move, which is the whole point of building something worth keeping.
When Cleanrooms Meet Real-World Demands
A cleanroom on paper is a controlled envelope: filtered air, positive pressure, strict gowning, and a particle count that stays beneath a threshold. On a Tuesday afternoon, though, a maintenance tech props open a pass-through to drag in a replacement motor, a rushed operator skips a tacky mat because the shift is behind, and a packaging line sheds fibers from cardboard that was never supposed to be there. Real-world demands don't pause for recertification schedules. They arrive as urgent work orders, new product introductions, and the quiet drift of habits that erode protocol long before an auditor notices.
The friction shows up in small decisions. A facility might spec ISO 7 but run a process that would happily live in ISO 8, while the real risk sits in a corner where condensation gathers on a chilled water line. Budgets can buy better HEPA coverage, but they can't buy compliance; people take shortcuts when monitoring feels punitive rather than diagnostic. Sensors drift, EM counts spike after a humid week, and suddenly the cleanroom isn't failing because the design is wrong but because the design never accounted for how the room actually gets used.
Closing that gap rarely means more rules. It means making the right behavior the easier one: placing wipe-down stations where hands naturally pause, designing pass-throughs that accommodate the actual carts, and treating brief excursions not as violations to hide but as data about where the cleanroom's boundaries are too rigid or too vague. A cleanroom that meets real-world demands is not the one with the strictest SOP. It's the one where the SOP, the layout, and the habits of the people inside finally stop pretending they're in different buildings.
Testing Beyond the Spec Sheet
A spec sheet is a snapshot taken under ideal conditions. It won't tell you that the battery sags after three weeks of daily charging, or that the fan develops a rattle once dust builds up behind the intake. We test for those unlisted failure modes because that's where the real ownership experience happens.
Bench tests start with the official numbers and then push past them. A pump rated for 8 bar gets run at 9.5. A hinge certified for 50,000 cycles gets opened and closed 50,010 times while someone watches for the first sign of slop. Deliberate overloading isn't about breaking things; it's about mapping the margin between claimed performance and the point where behavior becomes unpredictable.
Some observations never make it onto a datasheet. The feel of a rotary dial at the detent, the sound a latch makes when it engages, the way a display shifts color when viewed off-axis in warm light. These are the details that decide whether a product earns a place on a desk or ends up in a drawer, and we record them even when the numbers can't.
FAQ
It means combining precision machining, rigorous in-house testing, and a culture of continuous improvement so every splicer leaves the floor ready for demanding field conditions.
We use climate-controlled assembly areas, automated core alignment calibration stations, and record dimensional data for each unit to catch any drift before final inspection.
High-stability alloys for the frame, hardened glass optics, and industrial-grade piezoelectric actuators are selected not just for performance but for long-term reliability in varying environments.
Yes, the line includes flexible work cells that build to order, allowing adjustments to electrode geometry, fiber clamping, and software parameters without slowing standard production.
Every unit passes a multi-step test: calibration with reference fibers, splice loss measurement, tensile pull test, temperature cycling, and a final visual and functional audit.
By locking down critical assembly fixtures, using barcode-tracked components, and applying statistical process control on splice loss and alignment repeatability.
Operators rotate through each station and receive quarterly certification, which builds cross-functional skill and keeps workmanship consistent even as designs evolve.
Yes, sample units from each batch undergo extended cycling of clamps, motors, and heaters along with high-humidity and vibration exposure to simulate years of field use.
Conclusion
At the core of this facility is a simple but unforgiving requirement: give light an unobstructed path through a hollow-core fiber. That starts long before a splice ever happens. The fiber itself is drawn and handled in ways that keep the central void clean and perfectly round, because any contamination or asymmetry turns into scattering loss. Alignment stages on the fusion splicer repeat positioning to under half a micron, and operators learn to read the faint interference patterns that indicate a good match. It is slow work, closer to instrument making than assembly-line production. The quiet craft behind each splice means no two shifts feel identical, yet every splice has to meet the same invisible standard.
The hollow-core preform is built up layer by layer, each deposition pass adjusting the microstructure that will later guide light. Cleanrooms here are not just about particle counts; they are about controlling thermal drift, humidity, and vibration so that real-world splices behave as predictably as lab demos. When a unit reaches the test bench, the checks go beyond the datasheet: repeated thermal cycling, micro-bend stress, and long-duration loss stability under varying air pressure. Some fibers are deliberately contaminated at the facet before splicing to see how the machine recovers. That kind of testing catches failures that a spec sheet never mentions, and it is why these splicers leave the factory with more than a calibration certificate.
Contact Us
Contact Person: Mr XU
Email: [email protected]
Tel/WhatsApp: 86-25-85582828
Website: https://www.dvp.cn/en/