Non-Oriented Electrical Steel Top 10 Options for High Efficiency Applications
2026-09-19
High-efficiency applications leave little room for magnetic compromise. If you’re sourcing non-oriented electrical steel, the difference between a top-tier grade and an average one shows up fast in core loss, permeability, and long-term reliability. In this roundup, we’ve selected ten options that stand out for demanding motors, generators, and transformers—with a closer look at offerings from Jiangsu Baowu New Materials.
Core Loss Curves Worth a Second Look
Core loss data sheets tend to get a quick glance, a sigh, and a quiet burial in the project folder. But the shape of those curves hides more than a simple efficiency penalty. At low flux densities, the slope often flattens unexpectedly—hinting at eddy current suppression or measurement noise masquerading as physics. Ignore that region and you risk designing magnetics that run hotter than the numbers suggest, especially in light-load or standby modes where losses quietly accumulate.
Push further up the curve and the familiar knee appears, but not always where the manufacturer's summary implies. Material grade, lamination thickness, and even the direction of grain orientation can shift the break point by tens of kilohertz. A second look at the original plot, rather than the simplified equations, often reveals that your operating point sits closer to the steep loss cliff than you assumed. That margin you thought you had? It may be thinner than a layer of varnish.
There's also the matter of temperature. Core loss curves are usually measured at a single ambient condition, but real converters breathe hot air. The same material can lose half its headroom when the core temperature climbs forty degrees. Reading the curve again with that in mind—and not just trusting the headline watts per cubic centimeter—can turn a marginal design into one that survives the warranty period without a thermal camera argument.
When Standard Grades Start Holding You Back
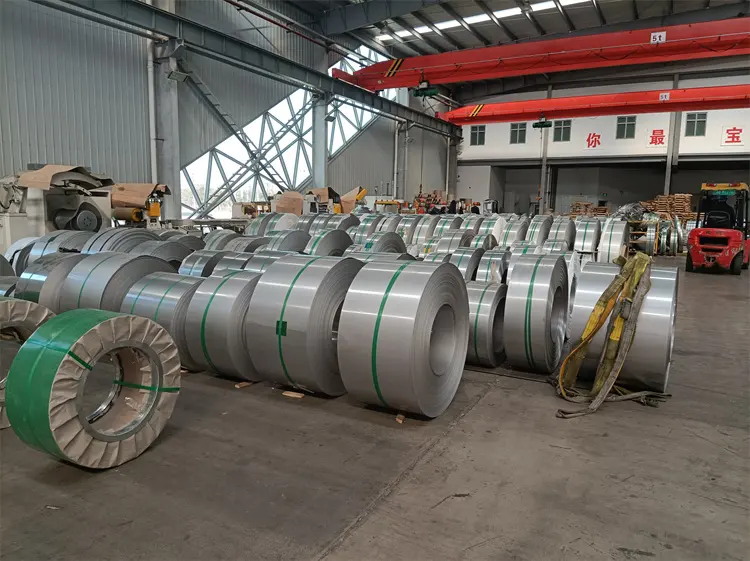
There's a quiet moment in many people's academic lives when the numbers stop feeling like a reflection of ability and start feeling like a ceiling. You might have spent years chasing the next decimal point, convinced that a perfect transcript would open doors. But then a project you poured your soul into gets overlooked because a single test score didn't match the rest of your profile. Or a conversation with a mentor reveals that the opportunities you've been missing weren't about your knowledge at all, but about a rubric that never quite fit the way you learn or create.
This shift often happens when real-world demands pull you away from the tidy logic of averages and percentiles. You notice that the people getting the most interesting work aren't necessarily the ones with the highest marks. They're the ones who can navigate ambiguity, push through failure, and bring a perspective that can't be captured on a bubble sheet. And yet, the system keeps asking for that same old number, treating it as a shortcut for trust rather than a single, narrow snapshot of a much larger story.
The trouble isn't that grades are meaningless. They can signal consistency and effort. But when they start to function as a filter for who gets to try, they quietly erase the skills that tests were never designed to measure. If you've started to feel boxed in by your transcript—like it's explaining away your potential instead of showcasing it—that's worth paying attention to. It might mean it's time to build a different kind of record, one that reflects the work you actually want to do, not just the work you've been scored on.
The Real Price of a Few Extra Efficiency Points
A few extra efficiency points rarely show up as a line item until the process breaks. The spreadsheet says the gain is free, but payroll, downtime, and turnover eventually pick up the tab. Pushing for that last bit of speed often removes the buffers that let people catch small problems before they become expensive ones.
Those points also have a way of turning into new obligations. Someone has to monitor the tighter tolerances, train replacements on the workarounds, and explain why the old method no longer applies. None of that shows up in the original cost-benefit math. A line running close to full capacity may look lean, but it leaves no room for a supplier delay or a sick team member.
Over time, the culture shifts. People stop suggesting improvements because each tweak makes the system harder to maintain. The real price is a quieter form of loss: fewer questions asked, less slack for judgment, and a growing reluctance to touch anything that might break. Walking away from a few efficiency points can be the smarter investment.
Thin Laminations, Thick Spec Sheets: What to Actually Check
When faced with a thick spec sheet for motor or transformer laminations, it's easy to get buried in dozens of pages. But the real performance hinges on just a few things: lamination thickness, material grade, and the type of insulating coating. Thin laminations reduce eddy current losses, but going too thin increases cost and lowers stacking factor. What you actually need to verify is whether the supplier provides true B-H curves for the specific grade, not just nominal data pulled from a brochure.
Don't fixate on thickness alone. Two stacks with the same lamination thickness can behave very differently depending on silicon content and annealing process. When you get samples, do a simple bend test to see if the coating flakes off, and measure the stacking factor yourself—it directly affects the effective cross-sectional area. Plenty of spec sheets look impressive until the physical parts arrive and fall short under load.
Another thing often overlooked is burr direction after stamping. If burrs face the air gap, they can cause localized hot spots and increased core loss. Ask for burr height data and confirm the overall dimensional tolerance after stacking. Thin laminations that are not aligned properly lose more performance than thicker ones because the relative misalignment is larger compared to the sheet thickness.
Heat, Speed, and the Grades That Handle Both
When a tool or component faces both extreme heat and rapid cycling, the material choice stops being a preference and starts being a survival strategy. Standard grades soften, oxidize, or lose dimensional stability long before the job is done. The alloys that thrive here tend to carry higher chromium and nickel contents, sometimes with molybdenum or tungsten, because those elements resist creep and scaling at temperatures where ordinary steel turns to butter. Speed adds another layer: fast thermal swings create stress gradients that can crack a lesser grade overnight.
For high-velocity applications that also bake under sustained heat, look beyond the usual 304 or 316. Grades like 310, 321, and certain duplex or precipitation-hardening variants earn their keep by holding tensile strength while other metals relax into failure. In turbine hardware, exhaust internals, or rapid-transfer furnace tooling, the right grade doesn't just tolerate the environment—it turns thermal and mechanical punishment into predictable performance. The trick is matching the grade to both the peak temperature and the rate of change, because a material that survives a steady 900°C may still crack if you slam it from cold to hot in seconds.
From Traction Drives to Home Appliances: One Steel, Many Trade-Offs
The same silicon steel that keeps a high-speed train gliding also spins the drum in a washing machine, but the demands couldn't be more different. Traction drives punish the material with punishing frequencies, elevated temperatures, and constant mechanical vibration, so manufacturers lean toward thinner gauges and higher silicon content to squeeze out every watt of loss. A home appliance motor, by contrast, rarely sees such abuse—its biggest hurdles are cost, noise, and the need to survive thousands of start-stop cycles without annoying the homeowner. The result is not one steel, but a family of grades that share a name and little else.
Push the silicon content up and you get lower eddy-current losses, but the steel becomes brittle and fights back during stamping, driving up tool wear and scrap rates. Traction engineers accept that trade-off because efficiency gains over a million kilometers outweigh the manufacturing headache. Appliance designers often pull back from that edge, choosing a slightly lossier grade that still punches cleanly and keeps the motor quiet enough for a midnight spin cycle. Coatings add another layer of compromise: a thin, inorganic film might protect against interlaminar currents in a locomotive, while a cheaper organic coating suffices for a refrigerator compressor that rarely breaks a sweat.
Even within a single appliance or drive unit, the "right" steel shifts with the operating point—torque at startup, cruising speed, or the short burst of a blender crushing ice. There is no universal winner, only a matrix of magnetic saturation, core loss, mechanical strength, and cost that designers must navigate without a compass. The steel that wins in a metro train's traction motor would probably be overkill and too brittle for a vacuum cleaner, yet both rely on the same underlying metallurgy, just bent to very different ends.
FAQ
Focus on core loss at the operating frequency and flux density, plus permeability under load. Grades with lower silicon content tend to punch more easily but have higher eddy current losses, so a balance between manufacturability and magnetic performance matters. Also check the coating quality because it affects interlaminar insulation and stacking factor.
Adding silicon raises electrical resistivity, which cuts eddy current losses, and it also reduces magnetostriction, lowering noise. But too much silicon makes the steel harder and more brittle, so stamping dies wear faster. Typical high-efficiency grades use between 2% and 3.5% silicon.
Grades equivalent to M270-35A, M300-35A, and M350-50A show up often in IE4 and IE5 motor designs. They offer a practical mix of low core loss at 50 or 60 Hz and acceptable punching behavior. Some manufacturers also switch to 0.35 mm or 0.30 mm thickness to reduce losses further.
Thinner laminations reduce the cross-sectional area for eddy currents to circulate, which directly lowers eddy current losses. At higher frequencies those losses rise sharply with thickness, so going from 0.50 mm to 0.35 mm or even 0.20 mm can make a noticeable difference in efficiency.
It can be used in smaller transformers, reactors, and rotating machines where flux direction is not fixed. Grain-oriented steel has superior properties along the rolling direction, but it is also more expensive and less forgiving in punching. For distribution transformers with a fixed flux path, grain-oriented is usually preferred, while non-oriented works well in less directional designs.
The coating provides electrical insulation between adjacent laminations, preventing large eddy current loops that would otherwise form across the stack. It also helps with punching lubricity and can improve corrosion resistance. A good coating should be thin enough to keep stacking factor high but robust enough to survive stamping and assembly.
Punching introduces plastic deformation and residual stress near the cut edges, which degrades magnetic properties locally. That can increase core loss by 10% to 20% if not addressed. Stress-relief annealing restores most of the lost performance, but it adds cost and time, so some designs use sharper tooling or laser cutting to minimize edge damage.
For a 0.35 mm high-grade non-oriented steel, core loss at 1.5 T and 50 Hz typically ranges from about 2.0 to 2.7 W/kg. Premium 0.30 mm grades can go below 2.0 W/kg, while standard 0.50 mm grades often sit around 3.0 to 4.0 W/kg. Exact values depend on silicon content and specific grade.
Conclusion
Many engineers skip past core loss curves too quickly, assuming the datasheet numbers tell the whole story. But when you plot loss density against frequency and induction, small differences between grades often widen under real operating conditions. Standard grades start holding you back once you push beyond typical 50/60 Hz sinusoidal excitation—think inverter-driven motors or high-frequency transformers. The real price of chasing a few extra efficiency points isn't just the material cost; it's also the design changes needed to handle thinner gauges, tighter stacking tolerances, and sometimes lower saturation. That trade-off rarely shows up in a simple cost-per-kilogram comparison.
Thin laminations look great on a spec sheet, but what you actually need to check is thickness consistency, surface insulation quality, and how the material behaves after punching or laser cutting—burr and edge damage can quietly erase the gains. Heat and speed are another filter: some grades hold their loss advantage at elevated temperatures, while others degrade faster under high-frequency ripple. From traction drives to home appliances, one steel rarely fits all. The top ten options for high-efficiency applications tend to cluster around a few practical compromises: low core loss at a specific frequency, acceptable yield strength for manufacturability, and stable performance across the thermal range the application actually sees.
Contact Us
Contact Person: Zoe Liang
Email: [email protected]
Tel/WhatsApp: 86 189 2128 6299
Website: https://www.baowuchina.com