Polyurethane Flame Retardant Distributor Qualities That Drive Consistent Product Performance
2026-11-16
Consistent polyurethane flame retardant performance rarely starts with the formulation alone—it starts upstream with the distributor. The wrong partner can make an approved chemistry look unpredictable; the right one keeps lot-to-lot variation off your production floor. At Fortune, that means rigorous specification control, transparent sourcing, and technical support that responds before small deviations become downtime. Here are the distributor qualities that actually protect your product consistency.
Batch Consistency That Makes Polyurethane Flame Retardant Performance Predictable
Polyurethane flame retardant performance hinges on one often-overlooked factor: how reliably each production batch matches the last. When the dispersion of the flame retardant additive varies even slightly, the resulting foam or elastomer can show unpredictable burn behavior. A batch that mixes too quickly may leave pockets of unprotected polymer, while an over-mixed batch can degrade the additive and reduce its effectiveness. This inconsistency forces manufacturers to over-engineer formulations just to stay within safety margins, wasting material and driving up cost.
Achieving predictable flame retardant performance starts with controlling the physical and chemical uniformity of every batch. Particle size distribution, moisture content, and viscosity must stay within tight tolerances. Advanced inline monitoring now allows real-time adjustment of mixing speed, temperature, and additive feed rates, catching drift before it becomes a failed lot. The goal is not merely to pass a single UL 94 test but to guarantee that the hundredth batch behaves like the first.
When batch consistency becomes a measurable process parameter rather than an assumed outcome, downstream benefits multiply. Molders can reduce the thickness of flame-retardant layers without risking compliance, because they no longer need to compensate for unknown variability. Certification bodies accept tighter statistical evidence from production data. In the end, predictable flame retardant performance is less about the chemistry of the additive and more about the discipline of making every batch identical.
Technical Support Teams Who Understand Foam, Coating, and Elastomer Processing
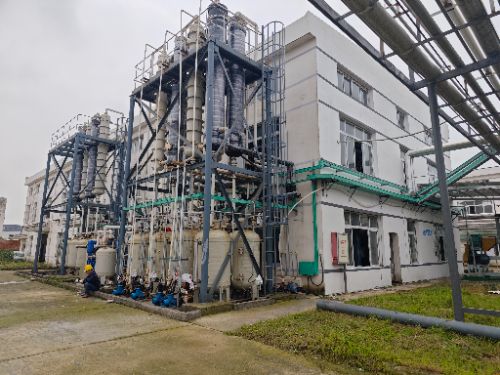
Our support staff includes people who have run foam lines, sprayed coatings, and compounded elastomers in production settings. When a foam cell structure shifts or a coating starts crawling on a substrate, they don't just read from a troubleshooting chart; they ask about line speed, humidity, tool temperature, and material lot changes because those details usually point to the real cause.
That background changes the conversation. Instead of generic advice, you get recommendations tied to your specific process: adjusting mixing energy for a polyurethane foam, staging solvent evaporation for a pressure-sensitive adhesive, or modifying cure time for a silicone elastomer without sacrificing tear strength. The team can also help with scale-up issues, like when a formula that worked on a lab coater behaves differently on a full-width production line.
Because they understand how these materials interact with equipment, they can spot potential problems before they become downtime. Whether it's resin buildup on a coating head, premature crosslinking in an elastomer feed system, or foam collapse caused by a minor temperature drift, the guidance is practical and based on time spent on real production floors.
Supply Chain Habits That Prevent Surprise Shortages and Rush Orders
Most surprise shortages begin quietly: a receiving clerk puts a pallet in the wrong bay, a buyer stretches a lead time by a few days, or a forecast ignores a customer's seasonal spike. Teams that rarely issue rush orders tend to walk the floor with a printed cycle count sheet for their top 80 SKUs every Monday, not just when finance asks for an audit. The count itself matters less than the immediate correction note attached to any variance above two percent.
Another habit is treating single-source and long-lead items as a separate planning bucket. Instead of letting the ERP system treat all parts with the same safety stock formula, these teams manually review the fifteen or twenty parts that could halt a shipment. They log supplier lead time changes in a shared sheet, adjust reorder points on the same day, and keep a small physical reserve for the two or three items with the longest history of delays.
The third habit is less about software and more about rhythm. Purchasing, receiving, and production leads hold a short Monday call to match inbound deliveries against the week's build plan. It is intentionally low-tech: one person reads out exceptions, another takes ownership for each item, and the group closes the loop by Wednesday. That cadence catches mismatches while there is still room to use standard freight instead of overnight shipping.
Compliance Documentation That Keeps Production Moving Without Interruption
Most plants treat compliance as a gate: finish the run, then check the paperwork. On a line that runs twenty-four hours, that gate becomes a bottleneck. A better approach is to make the record part of the operation itself. Operators verify lot numbers, enter line clearances, and sign off on in-process checks at the same workstation where they log downtime. The quality unit sees entries as they happen, not hours later. That means a small deviation gets documented and closed in the moment, while the line keeps moving within its validated limits.
The same logic applies to controlled documents. Rather than issuing a new SOP and waiting for someone to track down every printed copy, the system retires the old revision automatically. Supervisors get a notice when a work instruction changes, but they don’t have to stop the shift to retrain everyone from scratch unless the change actually affects how the task is performed. Review and approval happen alongside the daily work, so the document trail stays current without turning a routine update into an emergency.
During an audit, the difference shows up as time. Batch records, maintenance logs, training confirmations, and exception reports are already linked to the work order. Instead of pulling people off the floor to reconstruct a week of activity, a quality manager can retrieve the exact date, time, and sign-off for any step. That makes the documentation useful to the plant first and to the auditor second—which is usually the opposite of how compliance systems get built.
Custom Flame Retardant Blends That Fit Your Existing Line Conditions
A flame retardant blend only works if it runs clean on your equipment, and that means matching the line conditions already in place. Melt temperatures, screw speeds, die pressures, and cooling rates are not abstract numbers. They determine whether a compound fills the mold, holds tolerance, and reaches the required rating without scorching or plate-out. Rather than forcing an operation to adapt around a stock product, the additive package and polymer backbone can be selected to stay within the range your line already handles.
That often comes down to details most data sheets ignore. A grade that passes UL 94 on a lab plaque may still cause problems in a hot runner or a tight die gap. By working with your actual temperature settings, residence time, and regrind ratio, the formulation can be adjusted to prevent viscosity swings and surface defects. Additive choices, carrier resin melt flow, and char package level all move the compound toward a stable processing window without sacrificing flame performance.
What you end up with is not a universal product, but a compound fitted to your production reality. Trials go faster because the material is already close on day one. Operators do not have to relearn the line, and the quality team sees fewer burned spots, splay marks, or brittle weld lines. That is the difference between a supplier shipping pellets and a blend built for the way you actually run.
Shared Quality Data That Helps You Catch Problems Before Production
When quality data lives in disconnected spreadsheets and local drives, small signals get buried before anyone can act on them. A shared view changes that: every measurement, tolerance check, and material note from suppliers, engineering, and production sits in one place, so the team notices drift early instead of after parts are already on the line.
The real advantage is how quickly a shared record turns raw numbers into a story. Instead of reconciling versions or chasing missing test results, engineers can compare current runs against historical patterns, spot a supplier shift, or see that a fixture has been wearing out for weeks. That kind of context is what lets a team stop a bad batch while it is still cheap to fix.
Shared quality data also keeps everyone honest about priorities. When inspection results are visible across departments, a subtle dimensional trend in one component no longer stays hidden in a quality engineer's inbox. It becomes a shared prompt to adjust tooling, tighten a spec, or hold a shipment before the problem reaches the customer.
FAQ
A dependable distributor typically provides detailed technical documentation for each lot, including moisture content, particle size, and viscosity where relevant. They also maintain traceability back to the original production batch and can warn you when raw material sourcing shifts before it affects your line.
Consistency often comes down to how the distributor handles storage, repacking, and blending. If they control humidity during repacking, avoid cross-contamination between chemistries, and verify that each incoming lot matches the agreed specification, the flame retardant that reaches your mixer behaves the same order after order.
Look for incoming inspection against a written specification, retention samples for every shipped batch, and documented out-of-spec handling. It also helps if they have experience with phosphorus, halogenated, and intumescent systems, because each has different sensitivity to moisture, heat, and shear.
Even a fully formulated flame retardant can behave differently when combined with a new polyol, catalyst package, or filler. A knowledgeable distributor can help interpret viscosity changes, dispersion problems, or delayed cure and suggest adjustments without exposing your proprietary formulation.
Strong distributors limit the number of sourcing changes, quarantine incoming material until testing is complete, and communicate lead times honestly. They also maintain temperature-controlled warehousing for heat-sensitive products and keep detailed records linking your order to the original manufacturer's lot.
Request a plant audit or at least a detailed quality questionnaire, ask for recent certificates of analysis from multiple lots, and speak with current customers about how the distributor handled nonconforming material. A pilot order run across two or three separate lots can also reveal how consistent their handling and sourcing actually are.
Watch for reluctance to share certificates of analysis, frequent unannounced changes in country of origin, poorly labeled or damaged packaging, and vague answers about storage conditions. If a distributor treats flame retardants as simple commodities rather than functional additives, quality problems often follow.
Conclusion
A polyurethane flame retardant distributor earns its place on a production line long before a single drum arrives. It starts with batch-to-batch uniformity that lets foam, coating, and elastomer manufacturers run the same settings and still hit the same burn performance, density, and viscosity targets. When that consistency is paired with a technical support team that actually understands how additives respond to mixing speeds, mold temperatures, and cure profiles, the conversation shifts from troubleshooting after a failed batch to planning ahead of it. Those conversations matter because small formulation changes can ripple through physical properties, and a distributor who speaks the language of each process is far more useful than one who simply resells a product.
Behind that reliability sit quieter habits that keep production moving. Dependable inventory planning, clear communication about lead times, and realistic order expectations prevent the scramble of last-minute buying without falling back on vague promises. Compliance paperwork arrives ready for internal audits and customer sign-offs, not as a follow-up request. The strongest suppliers go further by offering custom blends matched to existing line conditions and by sharing quality data such as retention times, particle size, moisture levels, and thermal stability early enough for manufacturers to spot an issue before it reaches the mixer. Together, those qualities turn a chemical purchase into a predictable part of the manufacturing day.
Contact Us
Contact Person: WANG SIHAI
Email: [email protected]
Tel/WhatsApp: +86-13815295628
Website: https://www.fortunechemtech.com/index_en.html