Stainless Steel Carriage Bolt Supplier Checklist for High-Quality Fasteners
2026-10-12
When a stainless steel carriage bolt fails, the problem rarely starts with the bolt itself—it starts with the supplier you chose. A solid checklist can mean the difference between a fastener that lasts decades and one that rusts out months later. In this post, we break down the key points to look for, with practical insights from Wanluo to help you source high-quality fasteners with confidence.
Start With the Mill Test Report, Not the Price Sheet
Many buyers flip straight to the cost column when comparing steel suppliers. That habit quietly invites trouble. A mill test report tells you whether the material can actually survive the job—its chemistry, tensile strength, hardness, and heat treatment history. The price sheet only tells you what you'll pay today, not what you'll lose if a batch fails inspection or cracks under load. Starting with the MTR forces the conversation toward compliance and performance before money becomes the focus.
Think of the MTR as the material's passport. Every heat number traces back to a specific production run, so you can verify that the alloy matches your spec instead of hoping the warehouse shipped the right grade. Cheap quotes often come with missing or vague documentation, and that's where substitutions slip in. When you ask for the report first, you filter out suppliers who cut corners—and you stop chasing a low price that ends up costing more in rework, downtime, or rejected parts.
A useful practice is to read the MTR before you even compare prices. Look at the actual values, not just the grade name. Two plates of "4140" can behave very differently depending on how they were melted, rolled, and treated. If a supplier hesitates to share the report, treat that silence as an answer. The price sheet becomes useful only after the paperwork proves the material is worth quoting.
Thread Quality Tells You More Than the Head Stamp
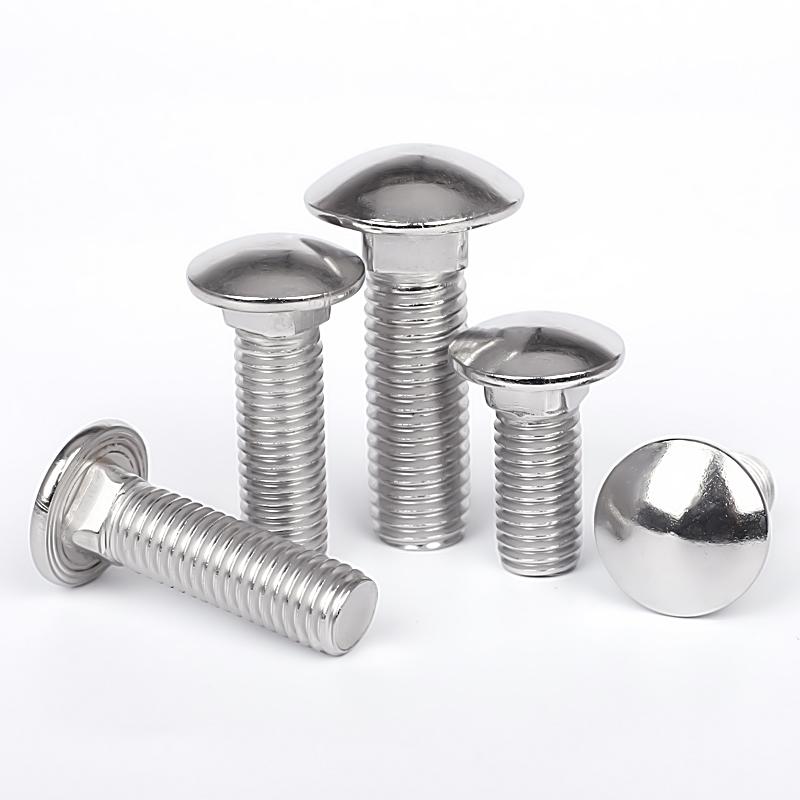
Head stamps on fasteners get a lot of attention because they identify grade and origin, but they are only surface markings. A poorly cut thread can pass a quick visual check while quietly compromising the entire joint. Run a nut down the thread by hand; if it binds, wobbles, or needs extra force at certain points, that inconsistency tells you far more about the fastener’s real condition than any stamped code.
Thread quality comes down to pitch accuracy, flank finish, and consistency of the major and minor diameters. These factors directly affect clamping force, fatigue life, and how smoothly parts go together. A bolt with clean, uniform threads will torque predictably and keep its load over time, while one with rough or shallow threads may feel tight at first and then fail without warning.
Before you trust a head stamp, inspect the threads under magnification or with a thread gauge. Look for galling, burrs, or uneven crests. If the thread form is off, no marking on the head can make up for the mechanical weakness that follows.
Passivation Is Not Just a Fancy Word for Clean
Many metal finishing shops still treat passivation as if it were a glorified degreasing step—run the parts through a citric or nitric bath, rinse, dry, and call it done. That mindset misses the entire point. Passivation is not about removing shop grime or visible soil; it is a controlled chemical process that alters the surface at a molecular level. When stainless steel is machined, traces of free iron get smeared into the surface. Left alone, that iron becomes the starting point for corrosion. A true passivation cycle dissolves that free iron and allows the chromium to react with oxygen, forming a thin, uniform oxide layer that actually shields the base metal. A clean part without that oxide layer is just a clean part waiting to rust.
The confusion often comes from the fact that passivation begins with cleaning. You cannot passivate a dirty part—oils, cutting fluids, and fingerprints block the acid from reaching the surface. But stopping after the cleaning step is like prepping a wall and never applying the paint. The cleaning removes the contaminants; the passivation removes the free iron and builds the passive film. Skipping or shortchanging the passivation step while claiming the part is “clean enough” leads to premature pitting, rust blooms in the field, and warranty claims. Worse, many shops run a quick dip in nitric acid and call it passivated without ever verifying the result. Without testing—copper sulfate, salt spray, or at minimum a water break test—there is no proof that the surface chemistry changed. A clean, shiny stainless part can still fail in service because the passive layer was never properly formed.
The practical takeaway is simple: treat passivation as an engineered surface treatment, not a housekeeping chore. Document the acid concentration, temperature, immersion time, and rinse quality. Validate the process with actual corrosion tests on sample parts, not just a visual glance. When someone says “we passivate in our cleaning line,” ask how they verify the oxide layer. If they cannot answer, you are likely paying for a fancy wash cycle, not passivation. And the difference shows up months later, in rust spots and leaked seals, long after the invoice has been forgotten.
Ask for Batch-Level Dimensional Data, Not a Sample
When you receive a dimensional report for a single sample part, you're essentially looking at a snapshot under ideal conditions. That part may have been measured right after tool setup, with fresh inserts, or hand-selected by the operator. It doesn't tell you what happens at hour six, when the machine has warmed up, coolant concentration has drifted, or a new batch of raw material runs slightly harder. Batch-level dimensional data means asking for measurements across the production run: multiple parts, multiple cavities, multiple time points. That's the only way to see whether the process stays centered between the tolerance limits or just barely survives a first article inspection.
A single out-of-context sample can hide systematic variation that only appears later. For example, an aluminum housing might pass a first-article check with a hole position error of 0.05 mm, well within a ±0.15 mm spec. But by part 400, tool wear has pushed that same hole to 0.13 mm, and by part 800 it's out. If you only asked for one or two samples from the start of the run, you'd never see that trend. Batch-level data — even something as simple as measuring every 25th part and plotting the deviations — exposes drift, step changes after tool changes, and differences between cavities in a multi-cavity mold.
So when you're writing a quality requirement or reviewing a supplier's inspection plan, don't settle for a golden sample report. Ask for raw dimensional values from a defined sampling interval across the entire batch, or better yet, for all critical dimensions on a statistically meaningful subset. Request the data in a spreadsheet or CSV, not a PDF summary with pass/fail checkmarks. This gives you the ability to run your own histogram, calculate actual Cpk, or compare batches over time. Suppliers that push back on this request often know their process is less stable than a single sample suggests.
A Supplier’s Lead Time Honesty Reveals Their Real Capacity
A supplier that tells you a lead time of six weeks when competitors are promising three isn't necessarily slower—they're often the only one being straight about their shop floor. Honest lead times come from someone who has actually looked at current orders, material availability, and bottleneck workstations before answering. The ones who instantly quote whatever you want to hear usually haven't checked anything, or worse, they know they can't hit it and are just trying to win the PO.
That honesty is a signal of production discipline. A supplier who gives a longer but reliable window is managing capacity instead of guessing at it. They've learned that late deliveries cost more than lost quotes, so they protect their schedule by not stacking jobs they can't run. Over time, that predictability becomes more valuable than a shorter date that slips twice.
If They Can’t Trace a Heat Number, Walk Away
A heat number is more than just a string of digits stamped on a pipe or plate. It's the only reliable link between the physical material and its mill test report—chemical composition, mechanical properties, heat treatment records, everything that proves it meets the grade you ordered. Without that traceability, you're not buying steel; you're buying a mystery.
Untraceable material often ends up on the market after being rejected elsewhere, mislabeled, or salvaged from unknown service conditions. Even if it looks fine on the outside, you have no way to verify what it actually is. In critical applications—pressure vessels, structural steel, process piping—that unknown can become a catastrophic failure, an audit nightmare, or a costly rework project months down the line.
So when a supplier shrugs off a request for heat numbers, or claims the documents are "somewhere else," don't negotiate. Walk away. Legitimate distributors and mills treat traceability as a non-negotiable part of the sale, and any hesitation on their end is a clear signal that the material isn't worth the risk.
FAQ
A trustworthy supplier will have mill test reports for each heat or batch, showing chemical composition and mechanical properties. For stainless steel, look for grades like 304 or 316 with traceable heat numbers. If they hesitate to share these documents, treat it as a red flag.
Pull ten bolts at random from different boxes and measure the shank diameter, length from under the head, and the square neck size with calipers. If you see more than a few thousandths of an inch variation, or the square neck doesn't seat snugly in a test hole, the lot likely has tooling wear issues.
A passivated finish is the minimum for marine environments. Passivation removes free iron from the surface and enhances the natural chromium oxide layer. For deck hardware or coastal construction, you can also request a pickled and passivated finish, which gives a duller gray look but better corrosion resistance than a bright polished surface.
Use a standard nut as a go-gauge and a slightly undersized thread gauge as a no-go check. The nut should spin on smoothly by hand with no wobble or binding. Also inspect under a bright light for torn, flattened, or overlapping threads near the point—those indicate dull cutting dies or poor thread rolling.
Ask for heat numbers stamped on each box or bag, not just on the pallet label. Clear, durable labels with grade, size, and lot number prevent accidental mixing. If the supplier uses color-coded inner bags for different lengths, even better—it saves time during picking and reduces the chance of sending the wrong fastener to a job site.
Request their latest capacity statement or a letter from their production manager stating weekly output for the specific diameter and length you need. Also ask for two or three current customer references in a similar industry. A quick call to those references often reveals more about real lead times and quality consistency than any brochure.
Each box should carry a lot number that ties back to the mill heat number and the production date. The supplier should be able to provide a traceability certificate mapping the finished bolts to the raw material heat, including any secondary processing like passivation or plating. For structural jobs, ask if they keep retained samples for at least two years.
Conclusion
A reliable stainless steel carriage bolt supplier earns trust long before the first shipment arrives. The mill test report carries far more weight than a price sheet, since it documents chemical composition and mechanical properties against the claimed grade—without that paperwork, you are buying a promise rather than a product. Thread quality is another silent tell: cleanly rolled, consistent pitch and smooth flanks indicate proper tooling and process control, while rough or uneven threads often point to worn dies or rushed production. Passivation matters too, but not as a buzzword. It must be a controlled chemical treatment that removes free iron and promotes a passive chromium oxide layer; if a supplier cannot describe their passivation process or verify it with test data, the clean surface may not resist corrosion the way stainless steel should.
Dimensional accuracy should never be judged from a single sample, because one good piece proves nothing about the batch. Ask for batch-level inspection records covering head diameter, shank length, square neck dimensions, and thread tolerances—suppliers who track and share this data demonstrate real process discipline. Honesty about lead times is equally revealing: a supplier who gives a realistic window and communicates delays early shows they understand their capacity, whereas one who promises the impossible just to get the order often underdelivers later. Finally, traceability is non-negotiable. Every batch should link back to a heat number, and that heat number should correspond to a mill test report. If a supplier cannot trace a fastener to its exact steel heat, they cannot stand behind its composition, and you should walk away. These checks separate consistently high-quality suppliers from those simply selling stainless hardware by appearance.
Contact Us
Contact Person: Shane
Email: [email protected]
Tel/WhatsApp: 8613357785029
Website: https://www.wanluohardware.com