Switchgear Tulip Contact OEM Key Factors for Choosing a Reliable Supplier
2026-09-15
Every switchgear assembly depends on components that rarely get the spotlight, yet none matter more than the tulip contact. Sourcing these precision parts from an OEM leaves little room for error: a marginal supplier can compromise thermal performance, shorten equipment life, and trigger costly field failures. So how do you filter out the noise and identify a partner you can trust? At MOLDVOLT, we've seen firsthand which criteria separate dependable manufacturers from the rest. In this guide, we break down the key factors—from material traceability to testing protocols—that should drive your decision.
Raw Material Traceability Separates Serious Suppliers
Most suppliers can tell you where their materials came from in broad strokes, but that's rarely enough when a batch fails or a customer asks hard questions. The ones worth keeping around maintain records that drill down to specific lots, harvest dates, and transport conditions. It's the difference between a shrug and a documented answer.
Traceability isn't just about paperwork for audits. It changes how problems get solved. When a contaminant shows up, a serious supplier can isolate the affected material within hours, not weeks, because their lot tracking doesn't rely on memory or a single overworked quality manager. That speed keeps recalls small and costs predictable.
You'll also notice it in how they talk about their upstream partners. Suppliers with real traceability can name their growers or refiners, explain why they chose them, and show how that choice stayed consistent across seasons. Vague sourcing claims tend to collapse the moment you ask for the actual chain of custody.
Dimensional Tolerances That Survive Real Operating Conditions
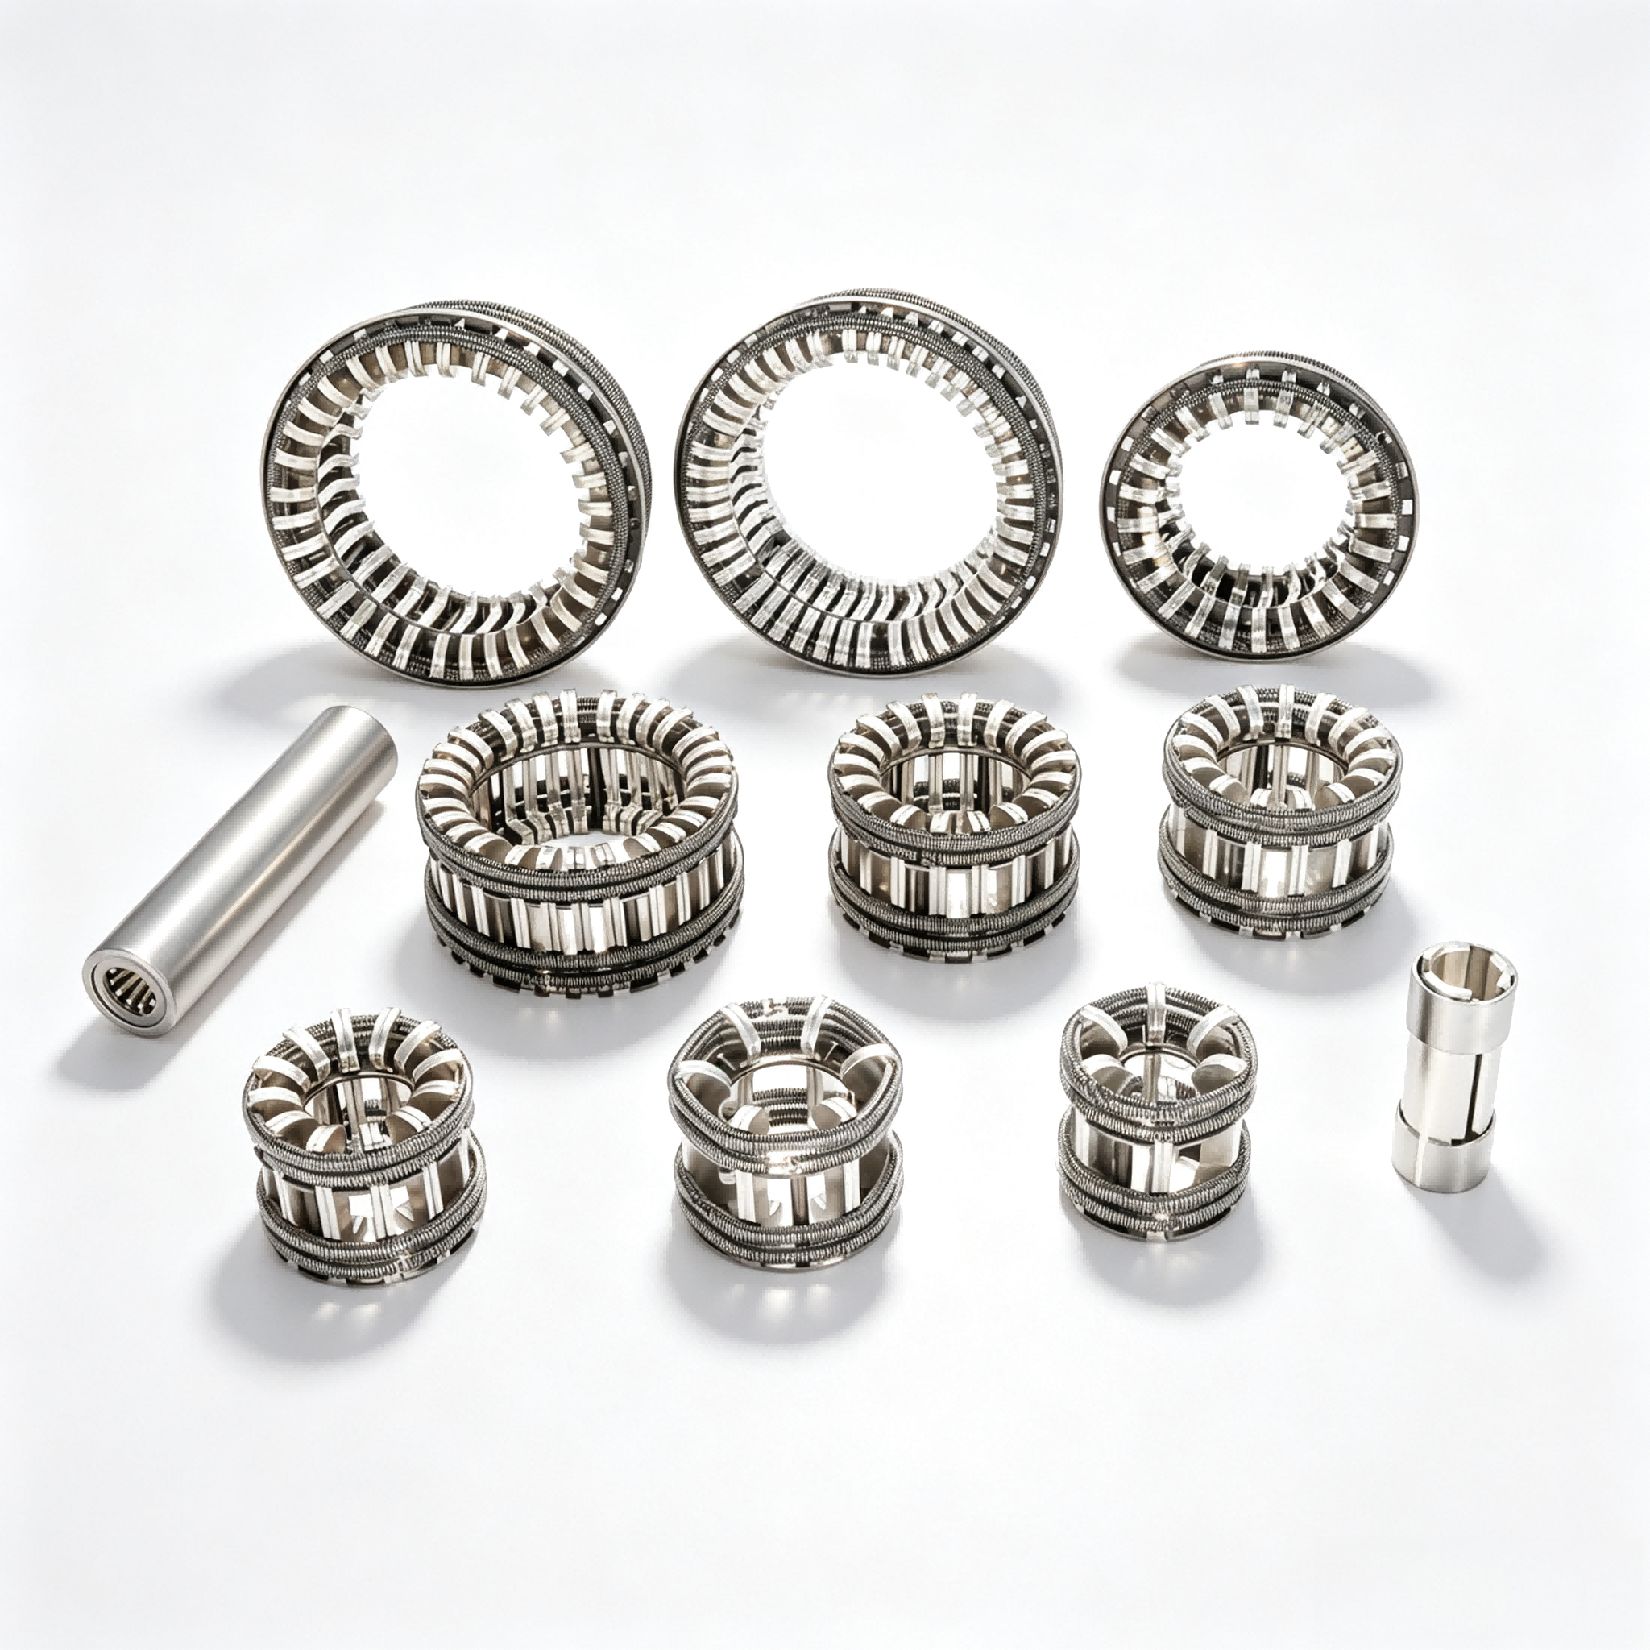
A tolerance printed on a drawing usually assumes a clean, 20°C room with zero load and perfect geometry. That picture dissolves the moment a part heats up, deflects under clamping force, or absorbs moisture from the air. Dimensional tolerances that actually survive in the field are built around these operational shifts, not static inspection numbers.
Consider a shaft running in a bronze bushing. The clearance that works at startup may close completely at operating temperature because aluminum housings expand faster than steel shafts. Likewise, a plastic gear's pitch diameter can grow by half a percent in humidity, enough to wipe out the design backlash. Real-condition tolerances come from measuring or simulating a component's hot, loaded, and worn state, then allocating variation only where function truly demands it.
A practical method is to map the tolerance zone as a band of acceptable performance, not a fixed pair of numbers. For a hydraulic spool valve, that means ensuring the spool-to-bore clearance never drops below the thermal lock-up threshold at maximum fluid temperature, nor opens enough to leak at minimum temperature. By testing prototypes under endurance cycles and field extremes, you can pin down the limits that keep assemblies quiet, sealed, and free-moving after thousands of hours. Those are the only tolerances worth putting on a drawing.
Plating Choices: Beyond Thickness to Bond Integrity
Most engineers fixate on plating thickness because it is easy to measure and spec. But in high-reliability applications, the real question is whether the plating will stay bonded when thermal stress hits. A shiny, uniform layer can hide weak adhesion at the interface, especially on alloys with high nickel or cobalt content. Pull tests and thermal shock cycling reveal failures that thickness measurements alone will never catch.
The bonding problem often starts before plating even begins. Residues from machining, passivation layers that form too quickly, or a rinse that leaves trace chlorides can all create a fragile boundary. When you then plate a hard metal over a softer substrate, differential expansion during soldering or operation applies shear at that boundary. If the adhesion is marginal, the plating lifts, cracks, or flakes—sometimes days after assembly, not during initial inspection.
A better approach is to treat bond integrity as a process variable, not a final check. That means qualifying the full surface preparation sequence for each base material, measuring adhesion with a repeatable method like a bend test or tape pull on a witness coupon, and tracking lot-level variation instead of relying on spot checks. Plating thickness still matters, but it is only one line in a longer story about how the coating survives real use.
Evaluating In-House Testing Without Marketing Fluff
A useful in-house evaluation begins with a plain list of what you actually measured, how many samples were involved, and which conditions changed between runs. If the summary only says “proven to work” or “industry-leading,” ask for the raw numbers behind those words. Real internal testing normally includes failures, borderline cases, and notes on what had to be adjusted before the results became stable.
Look for consistency between the claim and the method. A lab test on one batch in controlled conditions tells you very little about how a product behaves in daily use, yet many internal reports blur that line. The most credible write-ups name the limitations directly, mention repeated trials, and compare results against an unchanged baseline rather than a cherry-picked competitor.
Finally, treat the absence of detail as information. When an in-house report avoids sample sizes, environmental variables, or failure examples, it is often because the full picture weakens the marketing message. Ask the team to walk through the testing log instead of the polished summary. That conversation, not the brochure language, reveals whether the internal evidence can support the public promise.
Custom Tulip Contact Design: When Off-the-Shelf Falls Short
Off-the-shelf tulip contacts usually assume a narrow range of mating pin diameters, current densities, and insertion forces. When your design steps outside those assumptions—whether it's a non-standard pin size, higher continuous current, or a tougher thermal environment—the generic part starts to compromise. You might see uneven contact pressure across the fingers, localized hot spots, or premature wear from excessive deflection. Custom tulip contact design lets you set the number of fingers, their thickness, the spring arrangement, and the plating to match the actual mechanical and electrical load instead of settling for a close-enough fit.
Another weak point is the connection between the tulip and its carrier. Standard parts often rely on a fixed crimp or welded joint that doesn't suit every cable type or installation method. A custom design can incorporate a threaded stud, a compression fitting, or a different conductor transition that simplifies assembly and lowers contact resistance. Material selection plays a role too—off-the-shelf copper alloys may not balance conductivity and fatigue life well under frequent mating cycles or constant vibration. By specifying the alloy, heat treatment, and surface finish, you get a contact that maintains its spring force over time rather than gradually relaxing.
Predictable Lead Times Start With Process Discipline
Predictable lead times rarely come from heroic expediting or tighter promises. They emerge when teams stop treating each order as a unique event and instead apply the same basic rules to every job: clear ownership, defined handoffs, and standardized work steps. Without that structure, small delays quietly compound, and the end date becomes a guess rather than a commitment.
Discipline shows up most clearly in how exceptions are handled. When a team allows 'just this once' shortcuts under pressure, the process loses its ability to signal problems early. Keeping queue limits, batch sizes, and approval gates consistent may feel slower in the moment, but it removes the hidden variability that causes late deliveries. Over time, stable inputs create stable outputs.
The final piece is measuring what actually drives flow. Tracking cycle time, work in progress, and recurring blockers reveals whether delays come from the process itself or from outside noise. Teams that act on those patterns—instead of reacting to the loudest customer—can steadily reduce variation. At that point, lead times stop being a source of anxiety and become a natural result of disciplined execution.
FAQ
The tulip contact provides the primary current-carrying interface between the circuit breaker and the busbar or spout. Its multi-finger design maintains consistent contact pressure and low resistance even under thermal expansion and mechanical misalignment. A well-engineered tulip contact prevents hot spots and ensures reliable switching over thousands of operations.
OEM production means the contact is built to the exact dimensional, material, and performance specifications of the original switchgear design. Off-the-shelf alternatives often fail because tiny deviations in finger length, curvature, or spring force can alter contact resistance and lead to overheating. OEM ensures drop-in compatibility and preserves type-test certifications.
High-conductivity copper alloys are the standard, often with silver or tin plating to reduce oxidation and improve mating cycles. The base material needs good spring properties if the fingers rely on inherent elasticity, or it must pair with separate stainless steel springs. Avoid suppliers that use recycled copper with unknown impurity levels, as that can cause premature wear and higher contact resistance.
Silver plating offers excellent conductivity and low contact resistance, but it can tarnish in sulfur-rich environments. Tin plating is more corrosion-resistant but has limited maximum operating temperature. The plating thickness and adhesion are just as important as the material itself. A reliable supplier will document plating thickness and test adhesion under thermal cycling.
Look for compliance with IEC 62271-100 for circuit breakers and IEC 62271-1 for common requirements. The contact should be tested for temperature rise, short-time withstand current, and mechanical endurance. Suppliers who can provide type-test reports or equivalent certified test data from independent labs give much stronger assurance than those offering only dimensional checks.
They ask about your specific operating voltage, rated current, short-circuit level, and environmental conditions before quoting. They discuss spring force degradation, insertion depth, and alignment tolerances rather than just price and lead time. You also see evidence of reverse engineering or original design capability, along with a documented inspection plan for every batch.
Don't focus only on unit price. A cheaper contact that wears out faster or requires more frequent maintenance will cost far more over the switchgear's life. Consider the supplier's warranty, expected mechanical endurance, plating durability, and whether they provide lifecycle test data. Reliable suppliers often help you reduce unplanned downtime, which is the real hidden cost.
Conclusion
A reliable switchgear tulip contact OEM partner distinguishes itself long before the first batch arrives. Raw material traceability is non-negotiable — suppliers who cannot identify the exact heat or lot of their copper alloys put long-term conductivity and spring force at risk. Beyond chemistry, dimensional tolerances matter only if they hold under real load, not just on a calibration report. Tulip fingers that mate cleanly at room temperature can bind or lose contact pressure after thermal cycling and mechanical wear. Likewise, plating choices hinge less on advertised micron counts and more on bond integrity: a thick silver layer over poorly prepared copper will flake in service. Serious suppliers combine in-house testing with honest failure data, not marketing slides. Custom tulip contact design becomes critical when standard cages create hotspots or excessive insertion force, especially in high-current switchgear where contact resistance drives temperature rise.
Process discipline ultimately separates dependable OEMs from those with erratic delivery. Predictable lead times come from controlled blanking, forming, heat treating, and plating stages — not from chasing expedited orders. Look for suppliers who document their measurement methods, validate plating adhesion through bend or thermal shock tests, and maintain traceability from incoming bar stock to finished contact assemblies. When off-the-shelf tulip contacts fall short of your current rating or mechanical life requirements, a supplier with genuine co-design capability will propose revised finger geometry, altered contact pressure distribution, or alternative plating stacks without overpromising. The key factors overlap: a supplier that controls raw material and process variability can also hold tighter tolerances and deliver repeatable lead times, making the entire switchgear assembly more predictable in the field.
Contact Us
Contact Person: Hellen
Email: [email protected]
Tel/WhatsApp: 86-13634205622
Website: https://www.voltcabinet.com