Top Aluminum Checkered Plate Manufacturers You Can Trust for Durable Tread Plate Solutions
2026-10-21
When your project depends on aluminum checkered plates that can handle constant foot traffic, heavy equipment, or slippery conditions, settling for a second-rate supplier isn't an option. Too many manufacturers cut corners on alloy quality or pattern depth, leaving you with tread plate that wears out faster than expected. That's why we've done the legwork to identify the names that actually deliver on durability—including Sanhe Steel, a brand that consistently earns its place among top-tier producers. In this guide, you'll meet the manufacturers worth your trust and learn how to spot the difference between genuine long-term performance and flashy promises.
Why 'Trusted' Means More Than a Supplier's Marketing Claims
A supplier can print the word “trusted” on a brochure, a website banner, or a sales deck without a single customer ever having relied on them in a meaningful way. The label itself costs nothing, which is exactly why it appears so often. Real trust, however, is not something a company declares—it is something they accumulate through repeated, verifiable actions over time. It shows up in how they handle a late shipment, how they respond when a batch fails inspection, and whether they proactively share documentation instead of waiting to be asked.
One of the clearest signals of genuine trust is a supplier's willingness to open their operations to scrutiny. That might mean inviting a prospective client to tour the facility, sharing third-party audit reports without redaction, or providing direct contact with current customers who can speak to both strengths and weaknesses. Marketing claims are polished and one-directional; operational transparency is messy but informative. A supplier that only offers carefully curated testimonials and glossy case studies is telling you they prefer control over honesty.
Trust also has a measurable side. Look at retention rates, repeat order frequency, and how many clients have stayed through difficult periods such as raw material shortages or logistical disruptions. Those numbers tell a story that no tagline can match. A supplier who has kept the same core customers for a decade, even when cheaper alternatives existed, has earned something that cannot be faked. That kind of trust is built on consistent delivery, fair conflict resolution, and a refusal to overpromise—none of which fit neatly into a marketing slogan.
Aluminum Alloy Choices That Actually Hold Up Under Foot Traffic
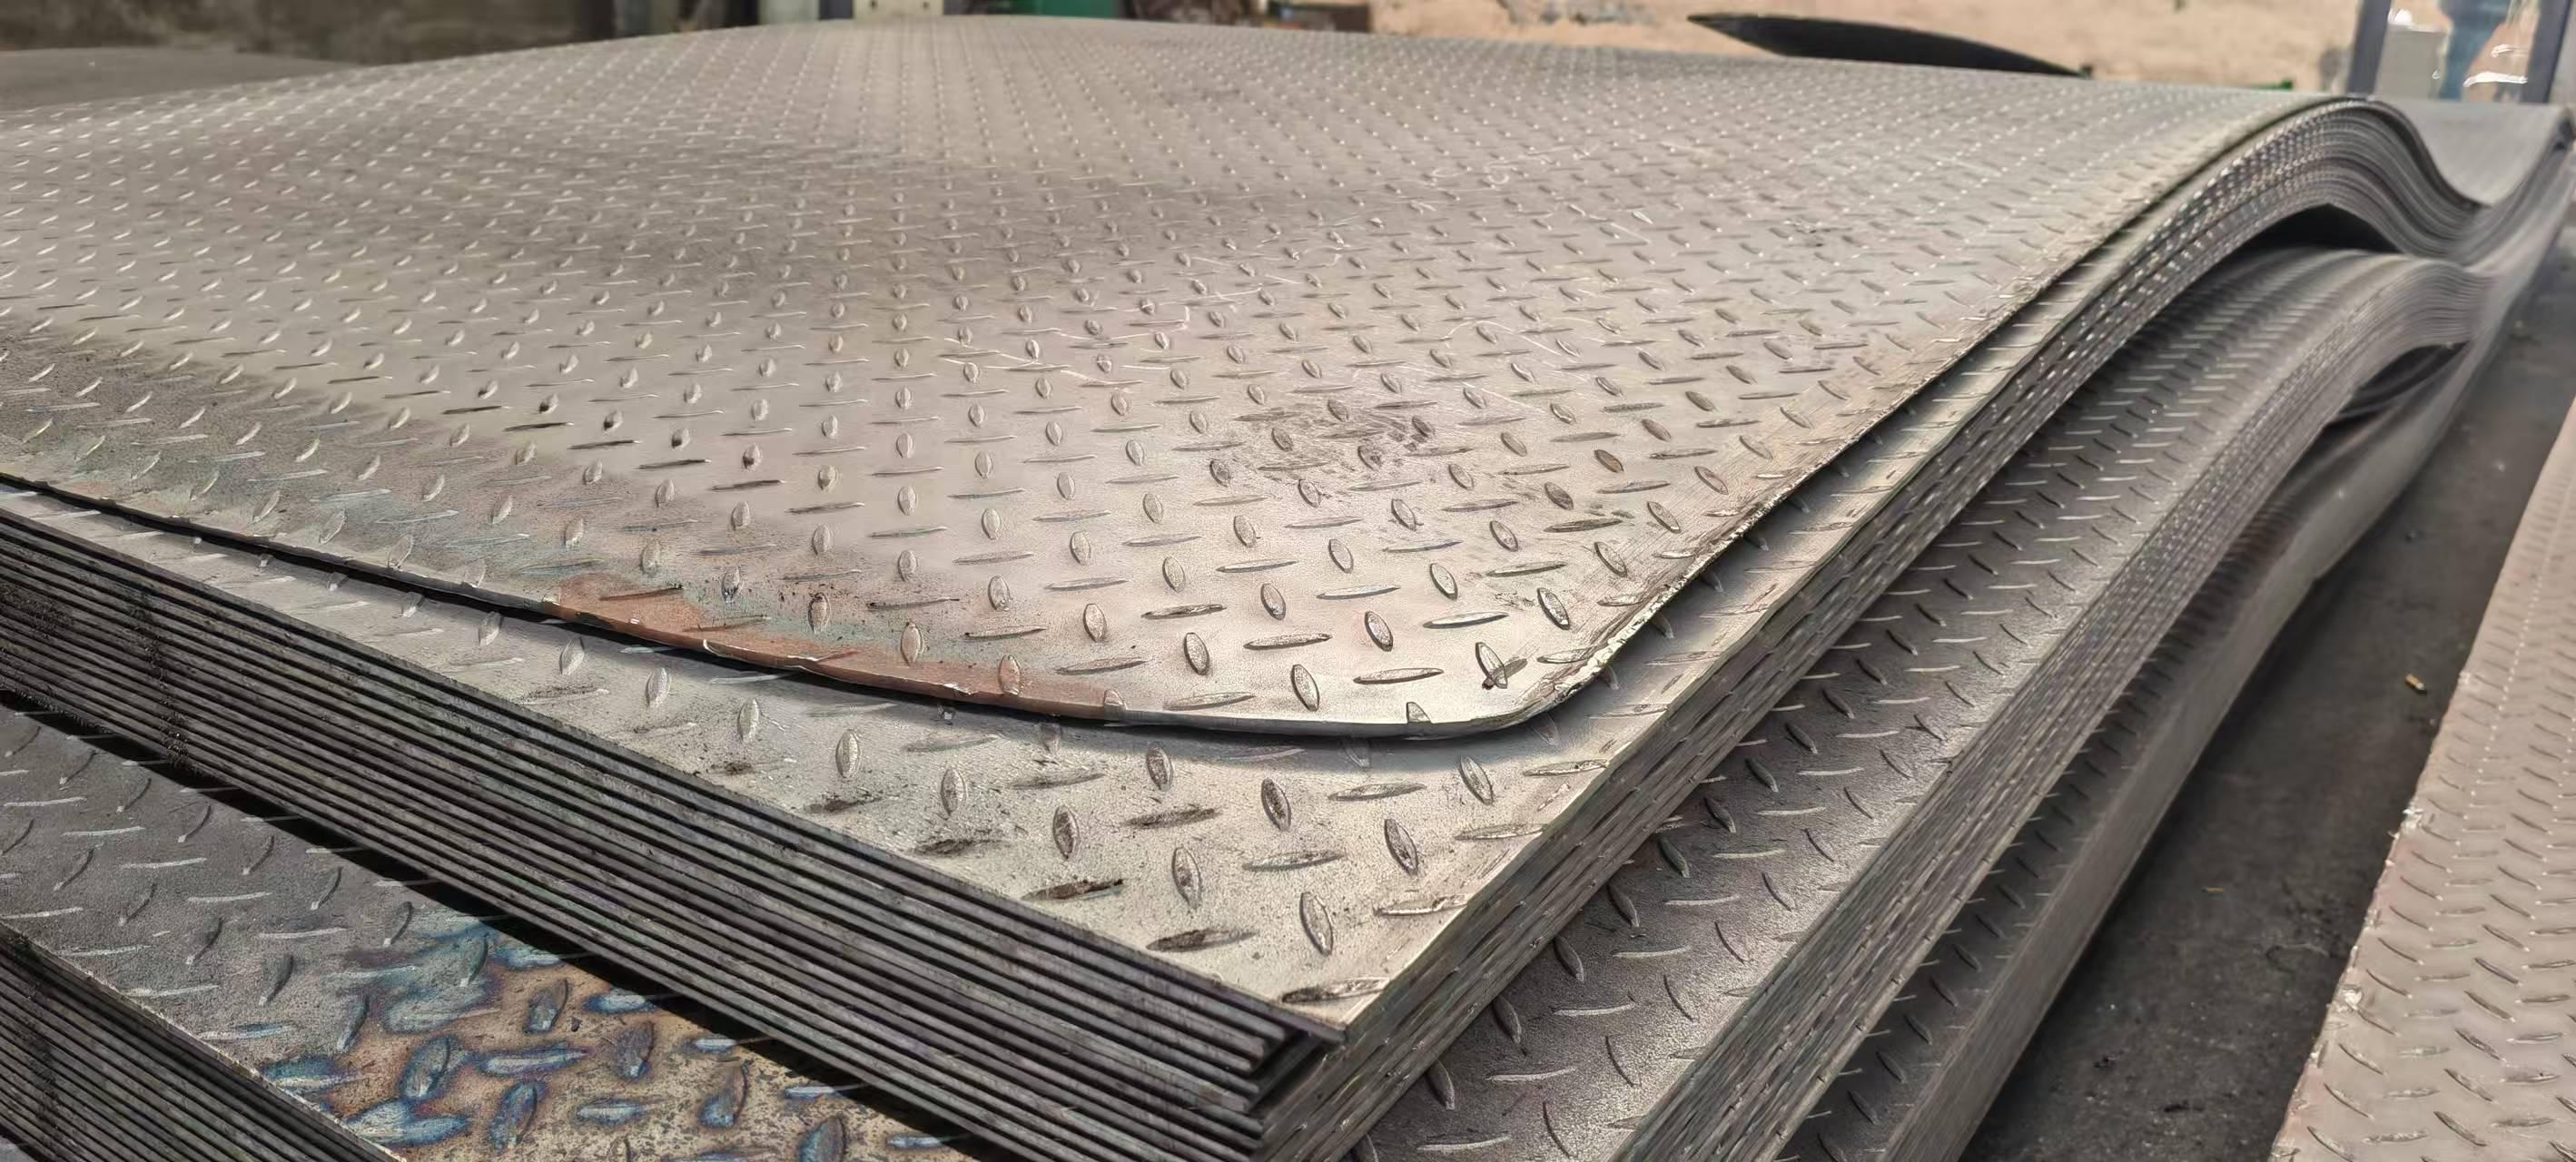
When foot traffic is heavy, the alloy's temper matters just as much as its base composition. 6061-T6 is a solid starting point because its higher magnesium and silicon content gives it better dent resistance than the softer 6063, which is often chosen for extruded handrails and door frames where surface finish matters more than raw strength. However, 6063-T5 can still work for light pedestrian zones if you pair it with a thick anodized layer to fend off scuffs.
For outdoor walkways or coastal boardwalks, 5083 or 5052 marine-grade alloys shrug off salt spray and moisture far better than 6061. Their trade-off is a slightly lower hardness, so they tend to show scratches sooner. A practical fix is to specify a brushed finish or apply a hard-anodized coating, which raises the surface hardness to a level that resists grit and dragging luggage without adding much weight.
If the installation will see constant rolling loads or sharp heels, look into 6082 or even 7075 for high-stress points like stair nosings and expansion joint covers. These cost more and are harder to machine, but they hold their profile longer under abuse. Another route is to stay with 6061 and add a durable powder coat over a chromate conversion layer, which hides wear and extends the metal's life in busy public spaces.
The Real Difference Between Diamond, Bar, and Five-Bar Patterns
A diamond pattern is a slow-burning reversal structure that forms after a strong move, price coils into higher highs and lower lows, then breaks out in the opposite direction—it traps traders on both sides before committing. Bar patterns, by contrast, live in the moment: a single candle or price bar tells you who controlled that specific session, whether buyers absorbed the selling or sellers swamped the buying. Five-bar patterns sit somewhere in between, stringing together a handful of bars to catch short-term momentum shifts without waiting for a full diamond to develop.
The practical gap comes down to timing and reliability. A diamond needs patience and often shows up at major turning points, while a bar pattern is noisy and best used as a confirmation filter, not a standalone trigger. Five-bar sequences are the trader’s quick read—they drop you into a micro-trend that might last a few hours, but they fail more often on higher timeframes. Knowing which one you’re actually looking at prevents the classic mistake of treating a two-bar pause like a full reversal or expecting a five-bar bounce to hold like a diamond breakdown.
Tolerances and Thickness: What Manufacturers Don't Always Tell You
The numbers on a spec sheet rarely survive contact with the real world. A sheet listed as 0.125 inches thick might measure 0.118 on one edge and 0.132 on the other, depending on how the mill rolled it and where the sample was cut. Most shops don't volunteer that their standard tolerance is ±0.005 inches until a part fails to fit, and even then, the conversation shifts to blaming your design rather than their process. Thickness variation isn't random noise—it follows a pattern tied to the temper, the alloy, and the time since the coil was unrolled. If you're designing around a single nominal value, you're already gambling.
What's rarely printed in the brochure is how much that tolerance stack compounds across a bend. A 10% variation in sheet thickness can translate into a 20% shift in the bend deduction, because the inside radius doesn't stay where you modeled it. Manufacturers may quote a ±0.003 inch capability for flat stock, but once you form a flange, the effective thickness at the corner becomes a moving target. Ask for actual measured thickness from the supplier's last three coils, not the theoretical gauge. If they hesitate, that's your answer.
Then there's the hidden cost of tight tolerances. Holding ±0.001 inch on thickness often doubles the price, not because the material is better, but because the mill has to sort and select—scrap rates climb, lead times stretch, and you pay for the privilege of being picky. Many designers specify a tighter tolerance than the application actually needs, simply because they don't know what the process can realistically deliver. A good fabricator will tell you that a looser tolerance with a well-designed gap or shim strategy is cheaper and more robust. A great one will send you the statistical distribution of thickness from their last run, so you can design to the median instead of the myth.
How Leading Tread Plate Suppliers Handle Custom Cutting and Finishing
Leading suppliers usually start with full sheets of common alloys and keep a mix of diamond, bar, and durbar patterns in stock. When a job calls for custom sizing, the shop floor pulls the closest match and runs it through a CNC plasma or waterjet table. Tolerances of +/- 1/16 inch are typical, though shops that cater to food processing or aerospace often hold tighter. The key is not just cutting the outline; it's planning the cut path so the raised pattern stays aligned and the finished piece doesn't warp, especially on thinner aluminum.
Finishing after the cut is where the differences show. A standard order might get a quick deburr and then move to packaging, but higher-end suppliers offer edge rounding, belt sanding to remove sharp corners, or a light etch before powder coating. For stainless or aluminum plates used in wet areas, the supplier may apply a non-directional finish or pass the piece through a timesaver to give it a uniform brushed look. Many shops also do custom punching or drilling in the same setup, which avoids a second handling step and keeps hole placement consistent with the pattern.
Signs a Checkered Plate Supplier Will Cut Corners on Quality
A supplier that quietly swaps standard thickness for thinner gauge plate is often hiding cost savings behind a spec sheet that never quite matches the delivered material. You might notice the checkered pattern feels shallower than samples you approved, or the edges show uneven rolling marks. When you measure several points across a sheet, the numbers drift far more than the mill tolerance allows. That kind of inconsistency doesn't come from normal production variation—it usually means the supplier is sourcing from secondary or rejected lots and hoping your team won't check.
Another red flag is the finish itself. Quality checkered plate has a crisp, uniform teardrop or diamond pattern with consistent height and spacing. If you see patchy areas where the pattern fades, or the surface feels oily but still shows early rust spotting after a short time in storage, the supplier may be skipping proper descaling, passivation, or protective oiling. Some will even mix batches from different mills, so one pallet looks bright and clean while the next has dull gray streaks and pitting.
Finally, watch how the supplier handles documentation and complaints. A supplier that cuts corners will push generic mill test certificates that don't match the heat numbers stamped on the plates, or they'll delay sending traceability records. If you ask about hardness, chemical composition, or bending tests and they only repeat marketing phrases instead of sharing actual data, that's a clear sign. Honest suppliers welcome verification; corner-cutters make it feel like an inconvenience.
FAQ
A dependable supplier should offer mill test certificates without being asked, state the exact pattern height tolerance on the quote, and provide a small cut sample before you commit to a full coil or bundle. Check whether they stock both 3003 and 5052 alloys, because a shop that carries only one grade may push you toward the wrong material just to move inventory.
For coastal or marine environments, 5052 is usually the better call because it resists saltwater corrosion far better than 3003. If weight savings and moderate corrosion resistance are enough, 3003 works well and tends to cost less. For heavy structural treads or industrial ramps, 6061 offers a stronger option, though it can be more prone to surface oxidation if left unpainted.
Measure the raised pattern height at several points with a depth gauge, not just by feel. Look for consistent spacing between diamonds or bars, and set the sample flat on a granite table to check for waviness. Rub a gloved hand hard across the surface to see if any loose oxide or burrs come off, which hints at poor rolling or handling.
Aluminum tread plate cuts a lot of weight, which helps with payload and fuel use, and it will not rust like plain steel. The trade-off is lower hardness, so dragging sharp metal objects across it daily will leave scratches faster. For trailers that carry moderate loads and face rain or road salt, aluminum is often the smarter long-term choice; for extreme abrasion or impact, steel may still win.
Yes, but the raised pattern makes fit-up slightly more work. Grind the pattern flat only where the weld will sit, and keep heat input moderate to avoid distorting the surrounding tread. Using 4043 or 5356 filler depending on the base alloy helps, and placing a copper backing bar behind the seam pulls heat away so the pattern stays crisp on the visible side.
Absolutely. Many buyers request bright or brushed finishes for architectural panels, powder coating in safety colors for ramps, or anodizing for extra surface hardness and corrosion resistance. A textured anti-slip coating can also be applied over the plate, but it changes the appearance and adds maintenance over time.
Stacking sheets without protective interleaving can press one diamond pattern into the surface below, leaving ghost marks that show up after anodizing. Using steel chains instead of nylon slings often gouges the edges. Keep the material dry and off concrete floors to avoid white corrosion staining, and store it at a slight angle so any trapped moisture runs off.
Ask for exact alloy and temper, pattern type and height, thickness tolerance, sheet size, quantity, packaging, and delivery lead time. Also confirm whether the price includes mill finish only or any protective film. A clear quote should state the inspection standard, such as ASTM B209, and whether partial bundles are allowed or if there is a minimum order per thickness.
Conclusion
Choosing a checkered plate manufacturer you can actually rely on starts with looking past glossy brochures and bold promises. The suppliers worth your time are the ones who openly discuss alloy selection—5052 and 6061 aluminum each behave differently under constant foot traffic, and a manufacturer that steers you toward the right grade for your environment is already proving their value. Tread pattern matters more than most buyers realize, too. Diamond, bar, and five-bar profiles aren't just aesthetic choices; they alter slip resistance, cleaning effort, and load distribution. A dependable manufacturer will explain these differences without pushing the most expensive option.
Thickness tolerance is another area where transparency separates serious producers from resellers. Reputable shops hold tighter dimensional ranges and will share inspection data rather than hiding behind vague spec sheets. Custom cutting and finishing—whether waterjet, shear, or edge rounding—should come with clear lead times and no surprise fees. Conversely, warning signs include inconsistent batch samples, reluctance to provide mill certificates, or vague answers about alloy temper. When a supplier treats your tread plate order as an engineering decision instead of a commodity sale, you've likely found one of the trustworthy manufacturers worth keeping on your shortlist.
Contact Us
Contact Person: Zoey
Email: [email protected]
Tel/WhatsApp: +86 15865577002
Website: https://www.sanhesteels.com