Top Mesh Fence Manufacturers in China: Who Leads the Industry?
2026-10-22
When it comes to securing perimeters or defining boundaries, the quality of your mesh fence can make or break the project. China has long been a global hub for fence manufacturing, but with hundreds of suppliers claiming excellence, finding the true leader isn’t as simple as a quick search. In this guide, we cut through the noise to spotlight the companies that consistently deliver durability, precision, and value — and we’ll also show you why Topfencesolar deserves a spot on your shortlist.
The engineering choices that separate serious mesh fence suppliers from the rest
A serious supplier begins with material traceability. They won't offer you a vague "galvanized wire" spec; they'll name the steel grade, the zinc coating weight in g/m², and the exact wire diameter tolerance. These numbers matter because a fence that sags after two winters usually failed in the spec sheet long before it failed in the field. Cheap suppliers hide behind marketing terms like "heavy duty," while engineering-driven suppliers hand you mill certificates and batch test reports.
Welding and weaving methods are another tell. Look closely at the intersections of a mesh panel: consistent heat signatures, minimal spatter, and uniform weld penetration indicate automated, calibrated production. Serious suppliers also control aperture deviation to under a millimeter across the panel, which prevents weak spots where livestock or intruders can pry. If the supplier can't tell you their weld shear strength or their aperture tolerance, they likely don't know their own product.
Post and footing design often separates the professionals from the amateurs. A serious supplier will ask about soil type, wind load, and expected lateral force before recommending a post schedule. They'll specify post wall thickness, embedment depth, and concrete collar diameter rather than offering a generic "one post every three meters" rule. They also consider thermal expansion and tensioning hardware, using turnbuckles or ratchet systems that keep the fabric taut without overstressing the top rail. These engineering choices cost a little more upfront but prevent the slow deformation, rust jacking, and anchor creep that plague cut-rate installations.
Why zinc-aluminum coatings have become the real durability benchmark
For decades, galvanized steel was the default answer to corrosion—until field data started telling a different story. Zinc-aluminum coatings didn't just edge out traditional zinc by a few years; they rewrote the expectations. The magic lies in the layered microstructure: aluminum migrates to the surface and forms a dense, ceramic-like oxide barrier, while the zinc underneath sacrifices itself more slowly. This combination delivers two distinct protection mechanisms that work in sequence rather than competing.
What catches engineers by surprise is how the coating behaves at cut edges and scratches. Pure zinc coatings tend to fail from the exposed steel outward, but zinc-aluminum alloys actively redistribute corrosion products to seal those vulnerable zones. During cyclic salt spray testing, panels with 55% aluminum content routinely outlast galvanized counterparts by three to five times—not because they're thicker, but because the aluminum-rich oxide layer resists the chloride attack that normally undermines the zinc's sacrificial action.
Field installations in coastal and industrial environments confirm what laboratory results hinted at: after ten years, zinc-aluminum coated structures show minimal edge creep and no significant underfilm corrosion. That real-world evidence, rather than marketing claims, has pushed specifying engineers and asset owners to treat this material not as an upgrade option, but as the new baseline for long-life steel components.
How leading Chinese factories hold tight tolerances on high-volume orders
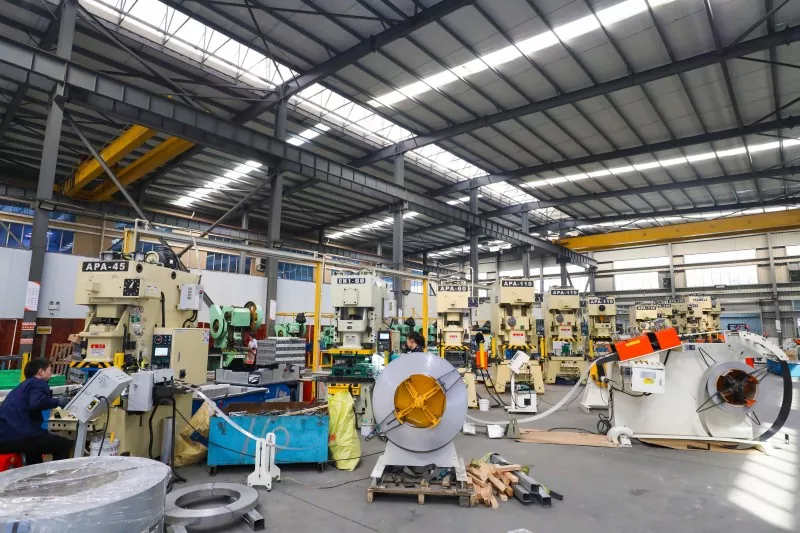
In high-volume manufacturing, achieving tight tolerances is less about buying the most expensive machines and more about building a process that self-corrects. Leading Chinese factories commonly embed automated inspection directly into the production line rather than relying on post-run quality checks. Data from vision systems and touch probes flows back to machine controllers, allowing micro-adjustments to be made before parts drift out of spec. For a batch of 50,000 units, this real-time feedback loop is often what separates consistent conformity from a costly sorting disaster.
A second differentiator is smart management of tool wear and thermal drift. Instead of waiting for dimensional deviations to appear in a final audit, these factories track usage hours and temperature fluctuations on critical equipment. Cutting tools are replaced on a schedule derived from historical wear curves, not guesswork. Metrology areas are climate-controlled, but measurements are also taken at the machine to catch drift when it starts. Line operators are given clear limits for minor offset corrections, which prevents small shifts from turning into large scrap batches.
Material consistency from upstream partners plays an equally important role. Top-tier Chinese suppliers often require raw stock and subcomponents to arrive with documented dimensional stability, so their own processes don't have to compensate for variable inputs. They also share live quality data with buyers, making tolerance conformance visible during the run rather than only at the end. This combination of incoming control, continuous in-process monitoring, and transparent reporting explains why high-volume orders from these factories routinely meet tolerances that many competitors would call too tight to quote.
Custom panel sizes, gauges, and finishes that don't stretch lead times
Odd-sized openings, extra-thick panels, a finish you haven't seen on a spec sheet in years—none of these need to trigger a delay. Our production setup treats custom dimensions as standard practice, not a special request that gets shuffled to the back of the queue.
Gauges run from feather-light to heavy-duty, and the switchover between them is built into the line rather than bolted on after the fact. That means a 16-gauge run doesn't take a back seat to a 20-gauge order just because someone in scheduling has to rethink the tooling.
Finishes get the same treatment: powder coat, brushed, anodized, even a one-off color match. The coating team works in parallel with cutting and bending, so the final look is already curing while the next batch is being formed. Lead times stay locked, no matter how far from the default box you ask us to color inside.
What global buyers actually inspect before approving a mesh fence factory
Serious importers rarely start with the production line. They walk the perimeter first, checking how raw wire is stored, whether zinc ingots sit in a locked cage or a dusty corner, and if rejected coils are clearly quarantined. A factory that can't keep its own yard orderly will not keep welding tolerances consistent. Buyers also ask to see the galvanizing bath operating, not just the spec sheet, because live temperature logs and dross removal routines reveal more than any certificate.
Next comes the weld itself. Experienced inspectors carry a pocket microscope and a pair of cutting pliers. They snap sample intersections from at least three different rolls, measuring nugget size and checking for burn-through or cold welds. They will also request line-speed data for the exact batch they watched, then compare it against the claimed daily output. A sudden speed increase often explains why the mesh looks perfect in the showroom but fails on a fence line six months later.
Finally, buyers test the coating in ways factories rarely advertise. They bend a strand around a mandrel, then dip it in copper sulfate solution to count pinholes per decimeter. They scrape the zinc layer with a calibrated knife and weigh the removed coating. They also inspect the packing area for moisture-absorbing desiccant and edge protectors, since sea freight condensation can destroy a perfect product. If a factory has no dedicated inspection room with retained samples from previous shipments, most global buyers will walk away without asking the price.
Manufacturers that project managers keep returning to for tough installations
In tight mechanical rooms and retrofit jobs with barely any clearance, project managers don't have time to experiment. They rely on a short list of manufacturers whose equipment has survived similar constraints before. These aren't always the biggest names in the catalog; they're the ones that keep tolerances when the mounting surface is uneven, the temperature swings hard, or the access is restricted to one side of the unit.
What separates these suppliers is how they handle the unexpected. A tough installation often reveals flaws that a clean spec sheet never shows, like a bracket that shifts under vibration or a wiring compartment that demands a third hand. The manufacturers project managers return to are the ones that offer real field support, pre-assembled subcomponents, and enough adjustment range to absorb site deviations. Some even send a technical rep to walk the site before the order is finalized, which saves hours later.
Over time, repeat business becomes a kind of shorthand. If a certain pump, drive, or enclosure made it through a cramped basement, a rooftop with 100-degree heat, and a retrofit with mismatched legacy piping, that record matters more than any datasheet. Project managers keep coming back because the installed base is proven, the documentation is written for actual installers, and the manufacturer's support line picks up when something still doesn't fit.
FAQ
A handful of names from Anping County in Hebei Province dominate the conversation. Companies like Anping Huijin Wire Mesh, Hebei Hengying, and Anping Yaqi consistently stand out because of their export volume, range of galvanized and PVC-coated panels, and long-standing relationships with overseas distributors.
It usually comes down to three things: the consistency of their wire diameter and coating thickness, how well they handle custom panel sizes without long delays, and whether they can produce the documentation for ISO or CE compliance without making you chase them. Price matters, but it's rarely the deciding factor for serious buyers.
It's not overhyped. Anping has been the center of China's wire mesh industry for decades, so you get a dense supplier base, specialized galvanizing plants, and experienced workers all within a short drive. That concentration lowers logistics costs and speeds up sample turnaround compared to factories elsewhere.
Reputable factories run in-line checks on wire tensile strength and zinc coating weight, then do random pull tests on welded joints before packing. Many also send pre-shipment photos or invite third-party inspection from firms like SGS or Bureau Veritas, especially for government or infrastructure projects.
The strongest categories are 3D curved panel fences, double-wire welded mesh fences, and temporary construction fencing. Beyond that, many manufacturers also do expanded metal and chain link, but the 3D and double-wire panels are where Chinese output really leads in both volume and finishing quality.
Yes, a visible shift toward automated welding lines and powder coating instead of traditional wet painting. Also, more factories are offering anti-climb designs with smaller apertures and hidden fixings, which appeals to municipal and utility buyers in Europe and North America.
Check whether the factory owns its own galvanizing line or outsources it, because that affects lead time and rust resistance. Ask for a sample with the exact coating spec, not just a standard one, and look at how they pack panels—good export packing uses steel pallets and edge protectors, not just loose bundles.
They can, but usually in niche areas like custom perforated screens or small-batch color matches. Large leaders win on price for standard panels and faster container loading, while smaller shops survive by being flexible and willing to take on odd specifications that big factories would reject.
Conclusion
The gap between a mediocre mesh fence supplier and a factory that survives brutal site conditions often comes down to engineering decisions made long before the first wire is drawn. In China, the manufacturers that keep earning repeat orders are the ones treating galvanized wire not as a commodity but as an engineered system. Zinc-aluminum coatings have quietly replaced traditional hot-dip galvanizing as the real durability benchmark because they resist corrosion at cut edges and weld points far longer, especially in coastal or high-humidity environments. At the same time, holding tight tolerances on high-volume orders separates serious players from the rest: leading factories use automated welding and inline diameter checks to keep mesh openings within a millimeter across thousands of panels, so installation crews don't waste time re-drilling or bending distorted sections.
Customization doesn't have to mean longer waits. The best-run Chinese factories keep a buffer of pre-slit wire and common panel sizes ready, allowing buyers to adjust heights, gauges, or PVC colors without pushing lead times from four weeks to twelve. Before approving a supplier, experienced global buyers tend to walk the production floor and look for things marketing brochures never mention: whether the zinc bath temperature is logged per shift, how rejected panels are marked and recycled, and whether the welding jigs are actually calibrated that week. These are the details that decide whether a mesh fence holds its shape after a decade of impact from livestock, forklifts, or coastal winds. That's why the same manufacturers keep showing up on shortlists for highway, solar farm, and warehouse perimeter projects—project managers return not because of price alone, but because the fence arrives straight, coated evenly, and ready to install even on tough sites.
Contact Us
Contact Person: Nancy
Email: [email protected]
Tel/WhatsApp: +86-13365923720
Website: https://www.topfencesolar.com/